
Chromic Acid Anodizing Type I
Anodizing & conversion coatings · Electrolytic bath
Type I and low-voltage Type IB chromic-acid anodizing form thin, corrosion-resistant oxide on aluminum with less fatigue penalty than thick sulfuric anodize.
Reference page — Type I anodize is not in the instant-quote configurator. Upload the part, name the finish in the notes, and an engineer quotes it with the part.
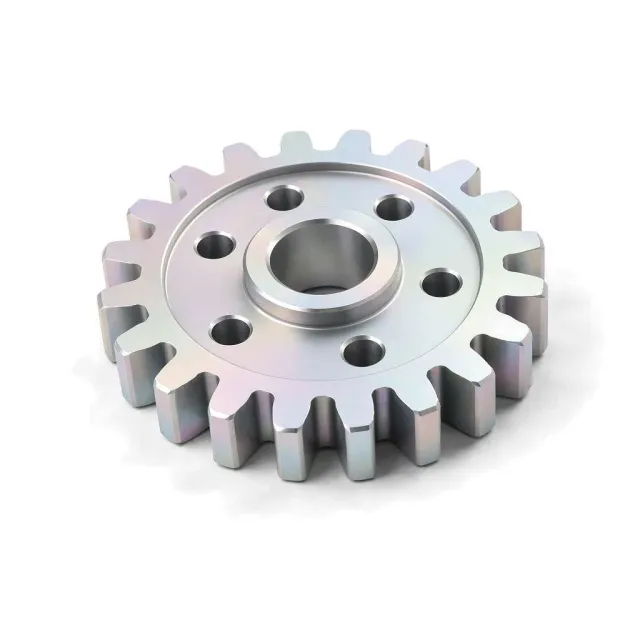
What is Type I anodize?
Aerospace drawings use MIL-A-8625 Type I or IB where trapped electrolyte, bonded structures, or fatigue sensitivity matter.
How it works
Aluminum is made anodic in a chromic-acid electrolyte while voltage is raised through a controlled cycle. The resulting oxide is thinner and more flexible than conventional sulfuric anodize, commonly about 0.5–7.5 µm depending on Type I or IB process and drawing requirement. Approximately half of the oxide grows outward. The porous film is normally sealed unless bonding requirements state otherwise. Chromic acid contains hexavalent chromium, so use is increasingly restricted despite its aerospace process tolerance.
Why specify it
- Thin 0.5–7.5 µm oxide limits dimensional change
- Lower fatigue debit than thick sulfuric or hard anodize
- Good corrosion protection after sealing
- Traditional aerospace choice for complex and bonded structures
Where it falls short
- Hexavalent chromium creates major regulatory burden
- Few decorative color options
- Lower wear resistance than Type II and Type III
- Not suitable for electrical contact surfaces
Type I anodize at a glance
Type I anodize is strongest on corrosion protection (71 of 100), at a premium cost.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
Type I anodize key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among anodizing & conversion coatings finishes.
- Thickness
- Approximately 0.5–7.5 µm depending on Type I or low-voltage Type IB process and drawing requirement.
- Hardness
- 150–300 HV — Typical thin chromic anodic film; not normally specified by hardness.
- Corrosion (salt spray)
- 336 h per ASTM B117, sealed, per MIL-A-8625 — Qualification performance is measured on standard specimens.
- Electrical
- Insulating
- Colours
- natural gray
- Appearance
- Thin translucent gray to slightly iridescent film.
Where Type I anodize sits among all finishes
Surface hardness (Vickers, log scale) against corrosion protection (salt-spray hours, log scale) for every coating FabDigit offers, one cloud per finish group. Type I anodize is highlighted; hover a dot for its name or open the full map.
Specifications for Type I anodize
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard, and US Government documents are free to download there.
| Standard | Type / Class | Thickness | Requirement / test | Status |
|---|---|---|---|---|
Anodic Coatings for Aluminum and Aluminum Alloys · DoD | Type I Class 1 | 0.5–7.6 µm | Chromic-acid anodize, non-dyed. · At least 200 mg/ft² unsealed (0.0215 g/dm²). · Coating weight; sealed corrosion test, ASTM B117, 336 h. | Supersedednow MIL-PRF-8625 |
| Type IB Class 1 | 0.5–7.6 µm | Low-voltage chromic-acid anodize, non-dyed. · At least 200 mg/ft² unsealed (0.0215 g/dm²). · Coating weight; sealed corrosion test, ASTM B117, 336 h. |
Test and related methods: ASTM B117 (Standard Practice for Operating Salt Spray (Fog) Apparatus).
Drawing call-out
CHROMIC ACID ANODIZE PER MIL-A-8625 TYPE IB CLASS 1, SEALED; MASK ELECTRICAL BONDING SURFACESPattern: ANODIZE PER MIL-A-8625 TYPE <I|IB|IC|II|IIB|III>, CLASS <1|2>, [COLOR], [THICKNESS FOR TYPE III], [SEAL], [MASKING]
Which materials take Type I anodize?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Used principally on wrought aerospace aluminum.
| |
| With care | Only aluminum DMLS/SLM parts can be processed; steel and titanium builds cannot. | |
| No | Brass is not anodized by this aluminum process. | |
| No | Copper alloys are not anodized by this aluminum process. | |
| No | Fused-filament polymers are incompatible with this process. | |
| No | Magnesium requires a magnesium-specific anodic or conversion process. | |
| No | Polymer powder-bed prints are incompatible with this process. | |
| No | Organic polymers cannot take this inorganic metal-finishing process. | |
| No | Photopolymer prints are incompatible with this process. | |
| No | Polymer powder-bed prints are incompatible with this process. | |
| No | Stainless steel is not anodized by MIL-A-8625 processes. | |
| No | This is an aluminum anodic process; steel does not form this oxide. | |
| No | Titanium uses a different anodizing chemistry. | |
| No | Zinc alloys are not anodized by this aluminum process. |
How Type I anodize is applied, and what it does to the part
- 1Clean
- 2Etch / deoxidize
- 3Rack and mask
- 4Chromic-acid anodize
- 5Rinse
- 6Seal if specified
- 7Inspect
| Dimensions | Allow approximately 0.25–3.75 µm outward growth per treated surface. |
|---|---|
| Build-up per side | 0.3–3.8 µm — Approximately half of the anodic oxide projects outward. |
| Masking | Usually needed. Mask electrical contacts, tight fits, threads, and bonding areas when unsealed oxide or bare aluminum is required. |
| Electrical | Insulating |
| Temperature limit | 80 °C (176 °F) continuous |
| Appearance | Thin translucent gray to slightly iridescent film. |
| Added lead time | 5–10 working days on top of the bare part |
Design rules for Type I anodize
What to decide on the drawing before the part goes to the finisher.
- State Type I or Type IB explicitly.The voltage cycle and resulting film differ.
- Confirm hexavalent-chromium authorization.Many programs restrict chromic-acid processing.
- Define sealed or unsealed condition.Bond adhesion and corrosion performance differ.
- Provide rack-contact and drainage locations.Anodizing requires current contact and complete rinsing.
Type I anodize versus the alternatives
Finishes engineers weigh against Type I anodize, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
Type I anodize this page | 71 | 49 | 28 | $$$ | 0.5–7.5 µm | — |
| 71 | 52 | 30 | $$$ | 3–8 µm | when a non-chromic aerospace thin anodize is approved | |
| 71 | 54 | 88 | $$ | 5–25 µm | when decorative color and broader availability matter |
The radar overlays Type I anodize with Boric-Sulfuric Acid Anodizing Type IC, its most common alternative — chosen when a non-chromic aerospace thin anodize is approved. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Chromic Acid Anodizing Type I is a premium-cost finish ($$$): more expensive than about 55 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 5–10 working days |
|---|---|
| RoHS | Conditional |
| Notes | Chromic acid contains hexavalent chromium; use requires regulatory and customer approval. |
What Type I anodize is used for
- Aerospace sheet structures
- Bonded aluminum assemblies
- Fatigue-sensitive brackets
- Complex parts with difficult rinsing geometry
Type I anodize — frequently asked
What is Type I anodizing?
Type I is chromic-acid anodizing under MIL-A-8625. It typically forms a thin 0.5–7.5 µm oxide for aerospace corrosion protection with limited dimensional and fatigue effects.
What is Type IB anodizing?
Type IB is a low-voltage chromic-acid variant. It remains a hexavalent-chromium process and must be called out separately from Type I.
Type I vs Type II anodize: what is the difference?
Type I uses chromic acid and is thinner, commonly 0.5–7.5 µm. Type II uses sulfuric acid, commonly 5–25 µm, and is better suited to dyed decorative finishes.
Does chromic acid anodizing add thickness?
Yes, approximately half the oxide grows outward. A 6 µm film adds roughly 3 µm per treated surface.
Is Type I anodizing RoHS compliant?
The process uses hexavalent chromium and normally cannot be treated as a straightforward RoHS-compliant choice. Program-specific exemptions and supply-chain declarations require review.
Other anodizing & conversion coatings finishes
 Chemical Conversion CoatingChem film is a thin chemical conversion coating for aluminum that improves corrosion resistance while retaining useful electrical conductivity.CorrosionHardnessCost$
 Hard Anodizing Type IIIType III hard anodizing forms a thick, dense aluminum-oxide layer for sliding, abrasive, and high-load service.CorrosionHardnessCost$$$
 Hard Anodizing Type III With PTFEPTFE hard anodize combines a 25–75 µm Type III oxide with a fluoropolymer impregnation or post-treatment to reduce friction.CorrosionHardnessCost$$$
 Magnesium Chemical Conversion CoatingMagnesium conversion coating reacts with magnesium alloys to improve corrosion resistance and paint adhesion with minimal buildup.CorrosionHardnessCost$$$
 Nitriding and QPQNitriding diffuses nitrogen into steel to create a hard wear-resistant case without depositing a conventional coating.CorrosionHardnessCost$$$$
 Plasma Electrolytic OxidationPlasma electrolytic oxidation, also called micro-arc oxidation, creates a thick ceramic oxide on aluminum or magnesium using high-voltage micro-discharges.CorrosionHardnessCost$$$$
 Sherardized Zinc CoatingSherardizing is a thermal-diffusion zinc treatment for steel fasteners and small components, standardized by ASTM A1059.CorrosionHardnessCost$$$
 Titanium Color AnodizingTitanium color anodizing grows a transparent oxide whose interference color identifies parts or provides a decorative finish without dyes.CorrosionHardnessCost$$
Compare every anodizing & conversion coatings finish side by side →