
Aluminum Chromium Nitride PVD
PVD hard coatings · Vacuum deposition
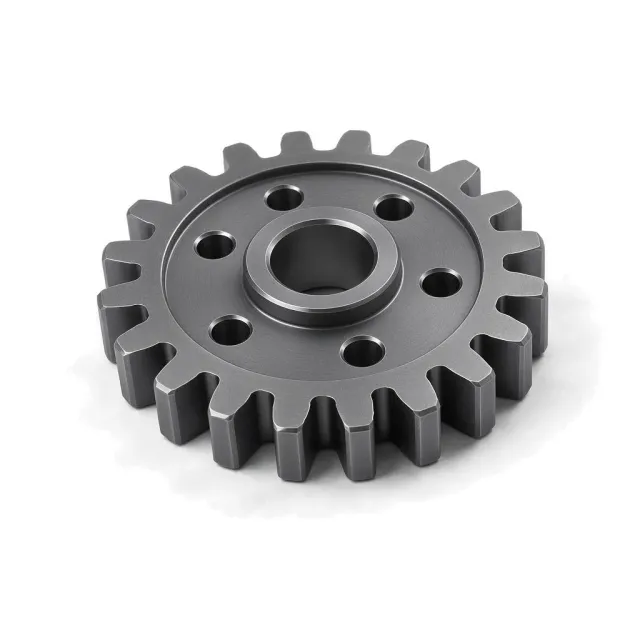
AlCrN is a dark grey PVD coating for high-temperature cutting, forming, moulding, and die casting tooling.
What is AlCrN PVD?
Around 3200 HV hardness and oxidation resistance near 1100 °C distinguish it from Ti-based coatings.
How it works
Aluminum and chromium are reactively deposited in nitrogen by arc or sputter PVD. Hot exposure forms protective aluminum- and chromium-rich oxides. The substrate must be conductive, hardened, clean, and stable through a typical 200–500 °C deposition cycle.
Why specify it
- About 3200 HV hardness
- Oxidation resistance near 1100 °C
- Good hot hardness without titanium
- Useful on cutting and mould tooling
Where it falls short
- Not a thermal barrier for the bulk part
- Hard film still needs hard support
- Arc droplets can affect polish
- Fits require 1–4 µm per-side allowance
AlCrN PVD at a glance
AlCrN PVD is strongest on surface hardness (93 of 100), at a high cost.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
AlCrN PVD key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among pvd hard coatings finishes.
- Thickness
- 2–4 µm
- Hardness
- 2,900–3,400 HV — Approximately 3200 HV typical.
- Electrical
- Semi-conductive
- Colours
- dark grey
- anthracite
- Appearance
- Dark grey to anthracite, satin to semi-gloss.
Where AlCrN PVD sits among all finishes
Surface hardness (Vickers, log scale) against corrosion protection (salt-spray hours, log scale) for every coating FabDigit offers, one cloud per finish group. AlCrN PVD is highlighted; hover a dot for its name or open the full map.
Specifications for AlCrN PVD
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard.
Drawing call-out
PVD COAT DESIGNATED SURFACES AlCrN, 2–4 µm THICK, DARK GREY; MAX PROCESS TEMPERATURE 500 °C; MASK FITSWhich materials take AlCrN PVD?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Hardened tool steel is preferred. | |
| Yes | Suitable for carbide tooling. | |
| With care | Use qualified activation and support hardness. | |
| With care | Possible with a qualified adhesion layer and a cycle that avoids excessive interstitial pickup. | |
| Limited | Low-temperature PVD only. | |
| Limited | Soft zinc-bearing alloy; decorative PVD is possible, not a wear-tool substrate. | |
| Limited | Soft copper alloys do not support a hard nitride; decorative films need a qualified adhesion layer. | |
| No | Melting point and reactivity exclude conventional PVD tool-coating cycles. | |
| No | Requires metallization and incompatible tool-coating heat remains a concern. | |
| No | Melting point is below typical PVD process temperature. |
How AlCrN PVD is applied, and what it does to the part
- 1Clean
- 2Ion etch
- 3Adhesion layer
- 4Reactive AlCrN deposition
- 5Inspect
| Dimensions | Add approximately 1–4 µm per coated side. |
|---|---|
| Build-up per side | 1–4 µm — Normal design allowance per coated side. |
| Masking | Usually needed. Mask precision fits, threads, and polished optical mould regions unless coating is specified there. |
| Electrical | Semi-conductive |
| Temperature limit | 1,100 °C (2,012 °F) continuous |
| Appearance | Dark grey to anthracite, satin to semi-gloss. |
| Added lead time | 5–10 working days on top of the bare part |
Design rules for AlCrN PVD
What to decide on the drawing before the part goes to the finisher.
- Confirm tool tempering temperature.The PVD cycle must not soften the tool.
- Polish before coating.The thin film reproduces substrate texture.
- Specify arc or sputter quality if polish matters.Arc droplets can print through.
- Compensate close fits.The film adds measurable size.
AlCrN PVD versus the alternatives
Finishes engineers weigh against AlCrN PVD, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
AlCrN PVD this page | 58 | 93 | 52 | $$$$ | 1–5 µm | — |
| 52 | 94 | 50 | $$$$ | 1–5 µm | a high-aluminum cutting coating is preferred | |
| 62 | 83 | 76 | $$$$ | 1–5 µm | greater toughness and silver appearance matter |
The radar overlays AlCrN PVD with Aluminum Titanium Nitride PVD, its most common alternative — chosen a high-aluminum cutting coating is preferred. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Aluminum Chromium Nitride PVD is a high-cost finish ($$$$): more expensive than about 91 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 5–10 working days |
|---|---|
| RoHS | Compliant |
| Notes | The deposited nitride is generally RoHS-compliant. |
What AlCrN PVD is used for
- Hot forging dies
- Die-casting tools
- Cutting tools
- Injection mould components
AlCrN PVD — frequently asked
AlCrN vs AlTiN: which handles more heat?
AlCrN is commonly rated near 1100 °C oxidation resistance, while AlTiN is often rated near 900 °C. Tool life still depends on the work material and cutting cycle.
How hard is AlCrN?
Typical hardness is about 3200 HV, with reported ranges around 2900–3400 HV. Test load and coating architecture affect the number.
How thick is AlCrN PVD?
A typical film is 1–5 µm, often 2–4 µm. Allow the thickness on every coated side.
Can AlCrN coat aluminum parts?
Only with a low-temperature qualified cycle that preserves temper. It is primarily specified on hardened steel and carbide tooling.
Is AlCrN suitable for moulds?
Yes, especially where hot wear and oxidation matter. The mould must be hardened and polished before the 1–5 µm coating is applied.
Other pvd hard coatings finishes
 Diamond-Like Carbon CoatingDLC is a family of black amorphous-carbon coatings used for very low friction and severe sliding wear.CorrosionHardnessCost$$$$
 Molybdenum Disulfide PVDMoS2 is a soft, dark-grey solid-lubricant coating selected for dry and vacuum mechanisms.CorrosionHardnessCost$$$$
 Titanium Aluminum Nitride PVDTiAlN is a violet-black PVD coating for high-speed and dry cutting.CorrosionHardnessCost$$$$
 Titanium Carbonitride PVDTiCN is a blue-grey PVD tool coating with about 3000 HV hardness and lower friction than TiN.CorrosionHardnessCost$$$$
 Titanium Diboride PVDTiB2 is a hard grey PVD coating chosen mainly to resist aluminum adhesion on cutting and forming tools.CorrosionHardnessCost$$$$
 Titanium Nitride PVDTiN is a gold, hard ceramic PVD coating for cutting tools, moulds, medical instruments, and decorative stainless hardware.CorrosionHardnessCost$$$$
 Tungsten Carbide Carbon PVDWC/C is a tungsten-containing hydrogenated amorphous-carbon coating, often written a-C:H:W, for sliding and rolling components.CorrosionHardnessCost$$$$
 Zirconium Nitride PVDZrN is a light-gold PVD coating used for decorative stainless products and for wear on non-ferrous cutting tools.CorrosionHardnessCost$$$$