
Decorative Nickel-Chrome Plating
Electroplating & electroless plating · Electrolytic bath
Decorative chrome is a multilayer system: copper when needed, one or more nickel layers, and a very thin chromium topcoat.
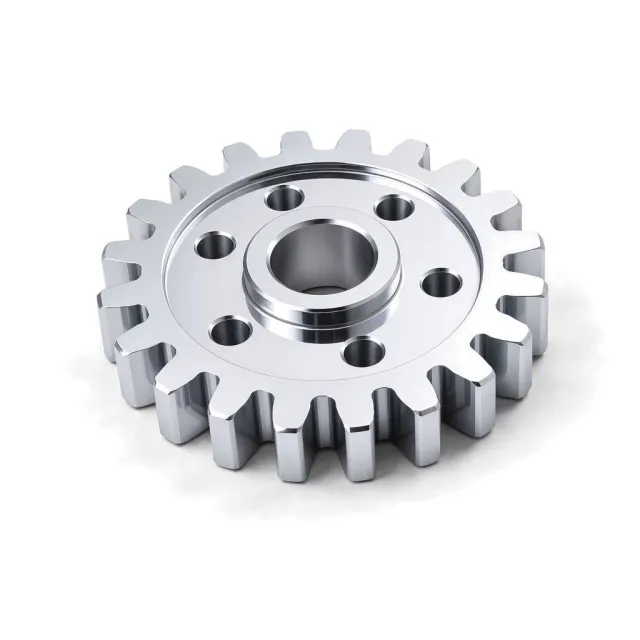
What is Decorative chrome?
ASTM B456 classifies service severity and layer combinations.
How it works
The substrate is polished and activated, then plated with leveling copper where needed and corrosion-protective nickel. A thin chromium electrodeposit supplies the blue-white color, tarnish resistance, and scratch resistance. The nickel provides most thickness and corrosion protection. Current crowding affects all layers, and deep recesses may remain thin unless auxiliary anodes and shields are used. Duplex nickel layers with different sulfur contents can create electrochemical protection before the microporous or microcracked chromium topcoat is applied.
Why specify it
- Mirror-bright blue-white appearance
- Chromium topcoat commonly 0.25–1.0 µm
- Nickel underlayers provide corrosion protection
- Suitable for metal and plateable ABS systems
Where it falls short
- Surface defects remain visible after plating
- Deep recesses have weak coverage
- Multilayer process adds cost
- Cr(VI) baths and nickel release face regulation
Decorative chrome at a glance
Decorative chrome is strongest on surface hardness (71 of 100) and cosmetic quality (95 of 100), at a premium cost.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
Decorative chrome key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among electroplating & electroless plating finishes.
- Thickness
- 0.25–1.0 µm chromium over a service-condition-dependent nickel or copper-nickel system
- Hardness
- 700–1,000 HV — Chromium topcoat hardness; the thin layer does not behave like thick hard chrome.
- Corrosion (salt spray)
- 96–500 h per ASTM B117 to red rust on steel, ASTM B456 SC2–SC4 nickel-chromium systems (typical) — Requirements depend on substrate and SC1–SC5 multilayer system; CASS (ASTM B368) is the usual acceptance test.
- Electrical
- Conductive
- Colours
- bright silver
- satin silver
- Appearance
- Bright, blue-white mirror or satin metallic appearance.
Where Decorative chrome sits among all finishes
Surface hardness (Vickers, log scale) against corrosion protection (salt-spray hours, log scale) for every coating FabDigit offers, one cloud per finish group. Decorative chrome is highlighted; hover a dot for its name or open the full map.
Specifications for Decorative chrome
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard.
| Standard | Type / Class | Thickness | Requirement / test | Status |
|---|---|---|---|---|
Standard Specification for Electrodeposited Coatings of Copper Plus Nickel Plus Chromium and Nickel Plus Chromium · ASTM | SC1 | ≥ 10 µm | Mild indoor service; steel Ni-Cr system uses 10 µm minimum nickel. · Thickness, adhesion, and appearance. | Active |
| SC2 | ≥ 15 µm | Moderate service; steel uses 20 µm bright nickel or 15 µm duplex nickel. · Thickness, adhesion, and applicable corrosion test. | ||
| SC3 | ≥ 25 µm | Severe service; steel Ni-Cr system uses 25 µm minimum duplex nickel. · CASS or specified corrosion test plus thickness. | ||
| SC4 | ≥ 30 µm | Very severe service; steel Ni-Cr system uses 30 µm minimum duplex nickel. · CASS or specified corrosion test plus thickness. | ||
| SC5 | ≥ 35 µm | Highest service category; steel Ni-Cr system uses 35 µm minimum duplex nickel. · CASS or specified corrosion test plus thickness. |
Drawing call-out
DECORATIVE COPPER-NICKEL-CHROMIUM PLATE PER ASTM B456, SERVICE CONDITION SC3, BRIGHT FINISH; SIGNIFICANT SURFACES AS SHOWNPattern: DECORATIVE <Cu-Ni-Cr|Ni-Cr> PER ASTM B456, SC<1|2|3|4|5>, CLASSIFICATION <SYSTEM CODE>, <APPEARANCE>
Which materials take Decorative chrome?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Common decorative and electrical substrate after cleaning. | |
| Yes | Excellent decorative plating substrate. | |
| Yes | Common over copper and nickel layers. | |
| With care | Requires zincate or equivalent activation plus a strike before the functional plate. | |
| With care | Metal AM parts can be plated after density, powder, and porosity review. | |
| With care | Requires activation and nickel strike. | |
| With care | Die castings need copper leveling and porosity control. | |
| Limited | Highly reactive; needs a qualified pretreatment and is rarely plated this way. | |
| Limited | Limited to plateable resins and specialized pretreatment.
| |
| Limited | Only if the resin is qualified for metallization; most SLA parts are not. | |
| Limited | Possible only with specialized activation; not a routine job-shop sequence. | |
| No | Fused-filament polymers are not a standard plating substrate. | |
| No | Porous nylon powder-bed parts are not a standard plating substrate. | |
| No | Porous nylon powder-bed parts are not a standard plating substrate. |
How Decorative chrome is applied, and what it does to the part
- 1Polish
- 2Clean and activate
- 3Copper plate if required
- 4Semi-bright and bright nickel plate
- 5Chromium plate
- 6Rinse
- 7Inspect appearance and corrosion class
| Dimensions | Design for total copper-plus-nickel-plus-chromium buildup, often 10–40 µm per side, not only the chromium thickness. |
|---|---|
| Build-up per side | 10–40 µm — Total system buildup is dominated by nickel and optional copper, not the thin chromium topcoat. |
| Masking | Usually needed. Mask threads, fits, hidden rack-contact zones, and surfaces where the full multilayer buildup is unacceptable. |
| Electrical | Conductive |
| Appearance | Bright, blue-white mirror or satin metallic appearance. |
| Added lead time | 5–10 working days on top of the bare part |
Design rules for Decorative chrome
What to decide on the drawing before the part goes to the finisher.
- Specify ASTM B456 service condition.The environment determines the required multilayer system.
- Polish before plating.A mirror deposit magnifies scratches and waviness.
- Place rack marks on hidden faces.Reliable current contact leaves a visible witness.
- Avoid deep narrow recesses.Poor throwing power leaves thin nickel and chrome.
Decorative chrome versus the alternatives
Finishes engineers weigh against Decorative chrome, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
Decorative chrome this page | 64 | 71 | 95 | $$$ | 0.3–1 µm | — |
| 51 | 55 | 78 | $$ | 5–25 µm | when a warm silver nickel appearance is acceptable | |
| 40 | 73 | 45 | $$$$ | 10–500 µm | when thick functional wear resistance is required |
The radar overlays Decorative chrome with Electrolytic Nickel Plating, its most common alternative — chosen when a warm silver nickel appearance is acceptable. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Decorative Nickel-Chrome Plating is a premium-cost finish ($$$): more expensive than about 63 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates cross-checked against US job-shop pricing. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 5–10 working days |
|---|---|
| RoHS | Compliant |
| Notes | Finished metallic chromium can comply, but conventional plating uses regulated hexavalent chromium; nickel release limits may apply to skin contact. |
What Decorative chrome is used for
- Automotive trim
- Plumbing fixtures
- Appliance controls
- Furniture hardware
- Plastic bezels
Decorative chrome — frequently asked
decorative chrome vs hard chrome
Decorative chrome is typically a 0.25–1.0 µm chromium topcoat over much thicker nickel. Hard chrome is commonly 10–500 µm of chromium for wear and is often finish-ground.
how thick is decorative chrome plating
The chromium itself is commonly about 0.25–1.0 µm. Total buildup can be 10–40 µm because copper and nickel underlayers provide leveling and corrosion protection.
why is nickel under chrome plating
Nickel supplies brightness, leveling, and most corrosion resistance. The thin chromium layer mainly adds the blue-white color, tarnish resistance, and surface hardness.
can plastic be chrome plated
Yes, plateable ABS and selected ABS/PC grades can be etched, catalyzed, electrolessly metallized, then copper-nickel-chrome plated. Total metallic buildup is much greater than the 0.25–1.0 µm chromium topcoat.
why does chrome plating peel
Peeling usually traces to contamination, passive oxide, poor activation, or incompatible substrate preparation. Casting porosity and flexing plastic can also break adhesion even when the topcoat looks acceptable initially.
Other electroplating & electroless plating finishes
 Black Nickel PlatingBlack nickel is a thin dark decorative electrodeposit, commonly applied over nickel, copper, brass, or zinc.CorrosionHardnessCost$$$
 Brass PlatingBrass plating co-deposits copper and zinc to give steel, zinc die castings, or copper alloys a yellow decorative surface.CorrosionHardnessCost$$$
 Bronze PlatingBronze plating deposits a copper-tin or related copper alloy for warm decorative color, antiquing, or selected functional bearing surfaces.CorrosionHardnessCost$$$
 Cadmium PlatingCadmium is a sacrificial, lubricious coating retained mainly for aerospace, defense, and legacy hardware.CorrosionHardnessCost$$$$
 Copper PlatingCopper plating is a conductive, ductile undercoat used for leveling, adhesion, shielding, and build-up.CorrosionHardnessCost$$
 Electroless Copper PlatingElectroless copper chemically deposits a conductive seed layer on catalyzed plastics and inside printed-circuit through-holes.CorrosionHardnessCost$$$
 Electroless Nickel PlatingElectroless nickel is an autocatalytic nickel-phosphorus coating with nearly uniform thickness on complex geometry.CorrosionHardnessCost$$$
 Gold PlatingGold plating supplies tarnish-free, low-resistance contact surfaces and decorative color.CorrosionHardnessCost$$$$
Compare every electroplating & electroless plating finish side by side →