
Plasma Electrolytic Oxidation
Anodizing & conversion coatings · Electrolytic bath
Plasma electrolytic oxidation, also called micro-arc oxidation, creates a thick ceramic oxide on aluminum or magnesium using high-voltage micro-discharges.
Reference page — PEO is not in the instant-quote configurator. Upload the part, name the finish in the notes, and an engineer quotes it with the part.
What is PEO?
It is selected for wear, dielectric, thermal, and corrosion performance beyond conventional anodizing, usually under a processor-specific specification.
How it works
The light-alloy part is immersed in an alkaline electrolyte and driven at high pulsed voltage. Once dielectric breakdown begins, many short-lived micro-discharges locally transform the growing oxide into hard crystalline ceramic phases. Commercial coatings commonly span 10–150 µm and include a dense inner barrier plus a porous outer layer that may be polished or sealed. Aluminum systems can form alumina-rich phases; magnesium systems form magnesium-oxide and electrolyte-derived compounds. Waveform, electrolyte, alloy, and post-seal dominate final properties.
Why specify it
- Commercial systems span roughly 10–150 µm
- Local ceramic phases can measure about 700–2,000 HV
- Treats both aluminum and magnesium alloys
- Can combine wear, dielectric, and thermal functions
Where it falls short
- No single universal PEO specification or chemistry
- Rough porous outer layer often needs sealing or finishing
- Edge effects and microdischarge intensity affect uniformity
- Higher cost and fewer suppliers than conventional anodizing
PEO at a glance
PEO is strongest on corrosion protection (70 of 100) and surface hardness (74 of 100), at a high cost.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
PEO key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among anodizing & conversion coatings finishes.
- Thickness
- Commercial aluminum and magnesium systems commonly use 10–150 µm; supplier-specific ranges are much narrower.
- Hardness
- 700–1,500 HV — Reported local ceramic-phase microhardness; effective coating hardness is lower because of porosity. 2000 HV values are literature extremes, not a drawing acceptance range.
- Electrical
- Insulating
- Colours
- white
- gray
- dark gray
- Appearance
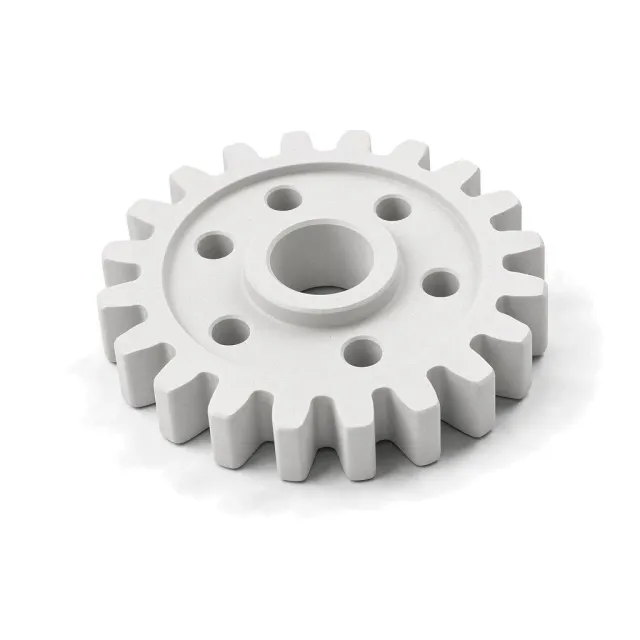
- Matte ceramic white, gray, or dark gray with a microtextured surface.
Where PEO sits among all finishes
Surface hardness (Vickers, log scale) against corrosion protection (salt-spray hours, log scale) for every coating FabDigit offers, one cloud per finish group. PEO is highlighted; hover a dot for its name or open the full map.
Specifications for PEO
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard.
Drawing call-out
PLASMA ELECTROLYTIC OXIDATION PER APPROVED PROCESS SPECIFICATION FD-PEO-001, 50 ± 10 µm, SEALED, FINAL HARDNESS 900 HV0.05 MIN; MASK THREADSWhich materials take PEO?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Many wrought, cast, and AM aluminum alloys can be processed after qualification.
| |
| Yes | A principal PEO substrate; sealing is usually important for corrosion.
| |
| With care | Aluminum or magnesium AM parts only, after porosity and powder review. | |
| Limited | PEO is technically possible but outside this aluminum/magnesium record's core offering. | |
| Limited | Some zinc PEO systems exist but are outside this aluminum/magnesium core offering. | |
| No | Brass is not a PEO substrate. | |
| No | Copper alloys are not PEO substrates. | |
| No | Fused-filament polymers are incompatible with this process. | |
| No | Polymer powder-bed prints are incompatible with this process. | |
| No | Organic polymers cannot take this inorganic metal-finishing process. | |
| No | Photopolymer prints are incompatible with this process. | |
| No | Polymer powder-bed prints are incompatible with this process. | |
| No | Stainless steel is not a standard PEO substrate in this offering. | |
| No | This PEO record covers valve metals (Al/Mg/Ti), not steel. |
How PEO is applied, and what it does to the part
- 1Clean
- 2Mask and rack
- 3Immerse in alkaline electrolyte
- 4Apply pulsed high voltage
- 5Rinse
- 6Seal or polish if specified
- 7Inspect
| Dimensions | Do not assume 50% outward growth; obtain the selected supplier's growth ratio and machine allowances for the specified 10–150 µm system. |
|---|---|
| Build-up per side | 5–100 µm — Growth ratio is process-dependent and cannot use the conventional anodize 50% rule universally. |
| Masking | Usually needed. Mask precision fits, threads, electrical contacts, and edges where high-voltage concentration is unacceptable. |
| Electrical | Insulating |
| Appearance | Matte ceramic white, gray, or dark gray with a microtextured surface. |
| Added lead time | 7–15 working days on top of the bare part |
Design rules for PEO
What to decide on the drawing before the part goes to the finisher.
- Qualify one supplier system before releasing dimensions.Growth ratio and porosity differ materially by chemistry and waveform.
- Specify post-seal or final grind.The as-processed outer layer is porous and rough.
- Round edges and provide robust rack contacts.High voltage concentrates at edges and contact quality controls arcing.
- State a test method with each property.Local HV values do not alone predict effective wear or dielectric life.
PEO versus the alternatives
Finishes engineers weigh against PEO, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
PEO this page | 70 | 74 | 35 | $$$$ | 10–150 µm | — |
| 71 | 61 | 50 | $$$ | 25–75 µm | when a standardized aluminum wear coating is adequate |
The radar overlays PEO with Hard Anodizing Type III, its most common alternative — chosen when a standardized aluminum wear coating is adequate. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Plasma Electrolytic Oxidation is a high-cost finish ($$$$): more expensive than about 84 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 7–15 working days |
|---|---|
| RoHS | Conditional |
| Notes | Many alkaline PEO systems avoid hexavalent chromium, but proprietary electrolyte and seal chemistry must be declared. |
What PEO is used for
- Light-alloy pump components
- Magnesium electronic housings
- Wear sleeves
- Dielectric heat-management components
PEO — frequently asked
What is plasma electrolytic oxidation?
PEO uses high-voltage micro-discharges in an electrolyte to turn aluminum or magnesium surfaces into ceramic oxide. Commercial coatings commonly range from 10 to 150 µm.
Is PEO the same as micro-arc oxidation?
Yes, micro-arc oxidation and MAO are common names for the same process family. Individual supplier chemistries and waveforms are not interchangeable.
PEO vs hard anodize: which is harder?
PEO ceramic phases are often reported around 700–2,000 HV, while Type III anodize is commonly 400–600 HV. Porosity and test method mean those numbers do not directly predict component wear life.
Can magnesium be plasma electrolytic oxidized?
Yes, magnesium is a major PEO substrate. The resulting oxide normally needs a qualified seal when corrosion protection is critical.
How thick is micro-arc oxidation?
Commercial systems broadly span about 10–150 µm, but one qualified process uses a much narrower band. The drawing should state thickness, seal, and supplier specification.
Other anodizing & conversion coatings finishes
 Anodizing Type IIType II sulfuric anodizing converts aluminum into a porous aluminum-oxide coating that can be clear or dyed.CorrosionHardnessCost$$
 Boric-Sulfuric Acid Anodizing Type ICBoric-sulfuric acid anodizing is a thin aerospace aluminum anodize recognized as MIL-A-8625 Type IC.CorrosionHardnessCost$$$
 Chemical Conversion CoatingChem film is a thin chemical conversion coating for aluminum that improves corrosion resistance while retaining useful electrical conductivity.CorrosionHardnessCost$
 Chromic Acid Anodizing Type IType I and low-voltage Type IB chromic-acid anodizing form thin, corrosion-resistant oxide on aluminum with less fatigue penalty than thick sulfuric anodize.CorrosionHardnessCost$$$
 Hard Anodizing Type III With PTFEPTFE hard anodize combines a 25–75 µm Type III oxide with a fluoropolymer impregnation or post-treatment to reduce friction.CorrosionHardnessCost$$$
 Magnesium Chemical Conversion CoatingMagnesium conversion coating reacts with magnesium alloys to improve corrosion resistance and paint adhesion with minimal buildup.CorrosionHardnessCost$$$
 Nitriding and QPQNitriding diffuses nitrogen into steel to create a hard wear-resistant case without depositing a conventional coating.CorrosionHardnessCost$$$$
 Sherardized Zinc CoatingSherardizing is a thermal-diffusion zinc treatment for steel fasteners and small components, standardized by ASTM A1059.CorrosionHardnessCost$$$
Compare every anodizing & conversion coatings finish side by side →