
Mechanical finishing & post-processing
Blast, brush, tumble, polish, grind; support removal, vapour smoothing, sealing, mould texturing.
Mechanical finishing
Blast, brush, tumble, polish, grind — changes texture and roughness, not chemistry. Usually the step before a coating.
| Finish | Suitable materials | Thickness (µm) | Lead time (days) | Relative cost |
|---|---|---|---|---|
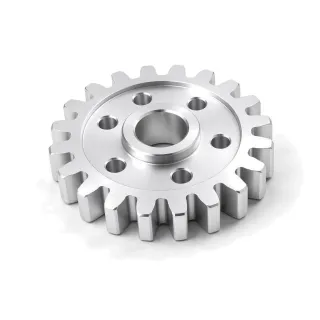 Aluminum Bright Dip Bright dipping is a chemical polishing pretreatment that levels microscopic peaks on aluminum to produce a reflective surface before anodizing. | Aluminum | No build-up | 3–6 | $$Standard |
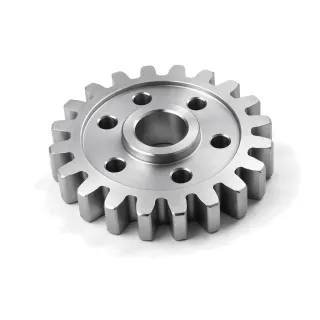 As Machined As machined is the baseline CNC condition with no secondary cosmetic finishing. | AluminumBrassCopper Alloy 6 more materials
| No build-up | 0 | $Budget |
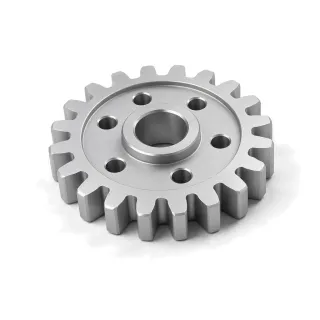 Bead Blasting Bead blasting propels spherical media at a surface to make a uniform satin or matte finish. | AluminumBrassCopper Alloy 11 more materials
| No build-up | 1–3 | $Budget |
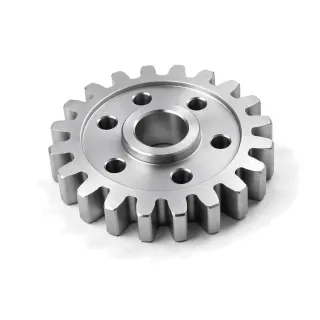 Brushed Finish Brushing creates a directional grain with abrasive belts, wheels, or pads. | AluminumBrassCopper Alloy 6 more materials
| No build-up | 1–4 | $$Standard |
 Deburring Deburring removes loose or sharp burrs left by cutting, punching, molding, or casting. | AluminumBrassCopper Alloy 6 more materials
| No build-up | 0–2 | $Budget |
 Edge Rounding Edge rounding deliberately replaces a sharp edge with a controlled radius or broad edge break. | AluminumBrassCopper Alloy 6 more materials
| No build-up | 1–3 | $Budget |
 Honing Honing precision-finishes bores with expanding abrasive stones and a controlled cross-hatch. | Stainless SteelSteel 7 more materials
| No build-up | 2–7 | $$$Premium |
 Lapping Lapping is a precision loose-abrasive process used to improve flatness, parallelism, and very fine roughness. | CeramicStainless SteelSteel 6 more materials
| No build-up | 3–10 | $$$$High |
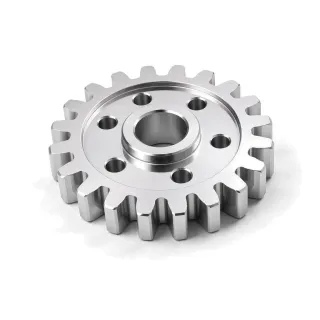 Mirror Polishing Mirror polishing removes visible directional scratches and buffs the surface to high specular reflectance. | BrassCopper AlloyStainless Steel 6 more materials
| No build-up | 3–10 | $$$$High |
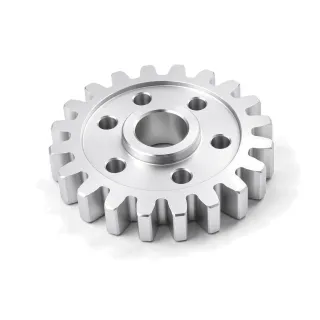 Polishing Mechanical polishing progressively removes surface peaks and scratches to produce a smooth glossy surface. | AluminumBrassCopper Alloy 6 more materials
| No build-up | 2–7 | $$$Premium |
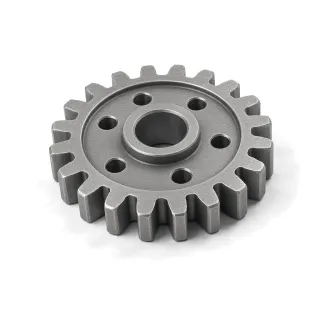 Sand Blasting Sand blasting uses angular abrasive to remove scale, rust, and coatings or to create a rough coating-ready surface. | BrassCopper AlloySteel 6 more materials
| No build-up | 1–3 | $Budget |
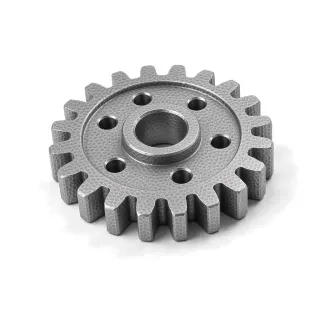 Shot Peening Shot peening bombards metal with controlled shot to create compressive residual stress and improve fatigue and stress-corrosion resistance. | AluminumNickel AlloyStainless Steel 6 more materials
| — | 3–7 | $$$Premium |
 Superfinishing and Isotropic Superfinishing Superfinishing removes grinding peaks from bearing and gear surfaces with very fine abrasive action. | Stainless SteelSteel 7 more materials
| No build-up | 3–10 | $$$$High |
 Surface Grinding Surface grinding uses a bonded abrasive wheel to generate precise flat surfaces. | Stainless SteelSteel 7 more materials
| No build-up | 2–7 | $$$Premium |
 Texture Finishing Texture finishing creates a controlled pattern on the mold so every molded part replicates it. | PolymerPolyurethaneSilicone 4 more materials
| No build-up | 5–15 | $$$Premium |
 Tumbling and Vibratory Finishing Tumbling and vibratory finishing are mass-finishing methods that deburr many small parts together. | AluminumBrassCopper Alloy 6 more materials
| No build-up | 1–3 | $Budget |
 Wet Blasting Wet blasting, vapor blasting, or vapor honing projects abrasive suspended in water to clean and satin-finish a surface. | AluminumBrassCopper Alloy 6 more materials
| No build-up | 1–4 | $$Standard |
3D-print & moulding post-processing
Support removal, vapour smoothing, sealing, degating, mould texturing — the steps that turn a printed or moulded part into a finished one.
| Finish | Suitable materials | Thickness (µm) | Lead time (days) | Relative cost |
|---|---|---|---|---|
 Chemical Smoothing Chemical smoothing applies a compatible liquid or vapor solvent to reflow or level selected printed polymers. | FDM (with care)MJF (limited)Polymer (with care) SLA (limited)SLS (limited) | No build-up | 2–7 | $$$Premium |
 Degating Degating removes the runner and gate from a molded or cast part. | PolymerPolyurethaneZinc Alloy 3 more materials
| No build-up | 0–1 | $Budget |
 Support Removal Support removal separates sacrificial print structures and cleans their attachment scars. | AluminumDMLS / SLMFDM 11 more materials
| No build-up | 1–5 | $$Standard |
 Surface Sealing Surface sealing fills connected pores in printed or cast parts with a compatible resin or sealant. | Binder JetMJFPolymer 11 more materials
| ≥ 0 | 2–7 | $$$Premium |
 Trimming Trimming removes flash, excess edge material, membranes, or sacrificial tabs. | PolymerPolyurethaneSilicone 5 more materials
| No build-up | 0–2 | $Budget |
 Vapor Smoothing Vapor smoothing briefly softens the outer skin of compatible powder-bed polymers so surface peaks flow together. | MJFSLS FDM (limited)Polymer (with care) | No build-up | 2–7 | $$$Premium |
Ranges depend on the substrate and process specification. Open a finish for test conditions and design limits. A dash means no value is listed.
Where mechanical finishes sit
These finishes change texture, edges or markings, not the hardness or the corrosion barrier of the surface — the base metal keeps its own figures — so they are not placed on the catalog's corrosion × hardness map. Compare them above by thickness removed or added, cost and lead time.