
Brushed Finish
Mechanical finishing · Mechanical
Brushing creates a directional grain with abrasive belts, wheels, or pads.
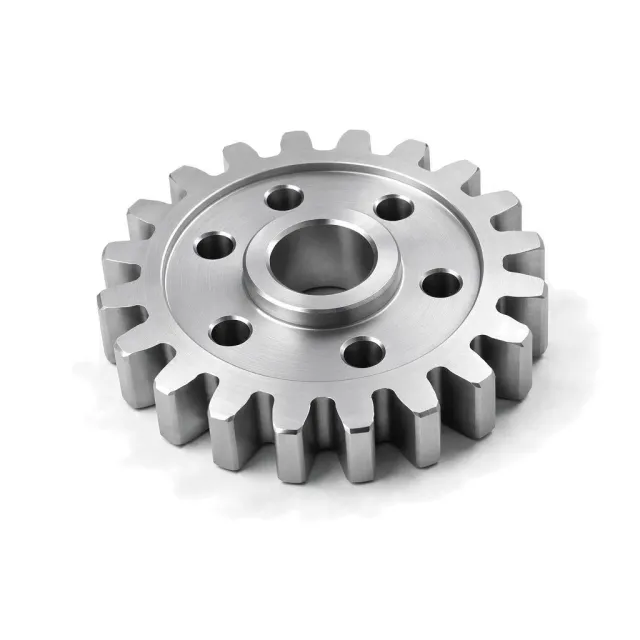
What is Brushed?
It is common on stainless and aluminum sheet and includes architectural hairline and commercial No. 4, No. 6, and No. 8 appearance classes.
How it works
The part passes under a coated-abrasive belt or wheel in one controlled direction. Abrasive in the 180–320 grit range commonly produces satin grain; progressively finer abrasive and buffing move toward No. 6 and reflective No. 8. ASTM A480/A480M identifies stainless sheet finish designations, but an approved sample is still essential because grit number alone does not fix appearance or Ra.
Why specify it
- Creates intentional directional grain
- Hides minor scratches along the grain
- Common 180–320 grit process window
- Typical Ra about 0.2–1.6 µm (8–63 µin)
Where it falls short
- Cross-grain scratches remain conspicuous
- Corners and recesses are hard to grain uniformly
- No. 8 requires polishing beyond ordinary brushing
- Abrasive cutting changes edges and thin features
Brushed at a glance
Brushed is strongest on cosmetic quality (75 of 100), at a standard cost. It adds little corrosion protection or lubricity. Surface hardness is not rated: the finish leaves the part's own surface.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
Brushed key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among mechanical finishing finishes.
- Thickness
- No coating; ASTM A480/A480M No. 4 typically Ra 0.4–0.8 µm (16–32 µin). Hairline and No. 6 sit finer; No. 8 is a polish, not a brush.
- Electrical
- Unchanged
- Appearance
- Directional satin grain; classes include No. 4 satin, No. 6 dull satin, No. 8 mirror-polished, and fine hairline.
Specifications for Brushed
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard.
Drawing call-out
BRUSH EXPOSED FACE PARALLEL TO LONG AXIS, 240 GRIT, ASTM A480/A480M No. 4 APPEARANCE, Ra 0.8 µm MAX; APPROVED SAMPLE CONTROLSWhich materials take Brushed?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Common for faceplates and consumer housings; scratches readily. | |
| Yes | Suitable; protect against smear and media embedment. | |
| Yes | Suitable; expect faster cutting and easier smearing than steel. | |
| Yes | Primary substrate for ASTM A480 directional sheet appearances. | |
| Yes | Suitable with contamination-controlled tooling or media. | |
| With care | Possible with non-sparking media and fire-safe dust control. | |
| With care | Bare brushed carbon steel needs subsequent corrosion protection. | |
| With care | Soft die-cast zinc cuts quickly and can embed media. | |
| Limited | Directional abrasion can frost or melt plastics; use only on rigid qualified grades. |
How Brushed is applied, and what it does to the part
- 1Level defects
- 2Brush in specified grain direction with 180–320 grit
- 3Progress to finer abrasive for class
- 4Clean residue
- 5Compare with approved sample and measure Ra
| Dimensions | Abrasive cutting removes a variable amount and softens exposed edges; do not brush precision fits or sealing lands unless stock allowance is specified. |
|---|---|
| Build-up per side | 0 µm — No buildup; abrasive stock removal is variable and should be excluded from precision faces. |
| Masking | Usually needed. Protect datums, sealing faces, lettering, and features that must retain sharp edges. |
| Electrical | Unchanged |
| Appearance | Directional satin grain; classes include No. 4 satin, No. 6 dull satin, No. 8 mirror-polished, and fine hairline. |
| Added lead time | 1–4 working days on top of the bare part |
Design rules for Brushed
What to decide on the drawing before the part goes to the finisher.
- Show grain direction on the drawing.Orientation dominates the visual match.
- Name the class and grit.No. 4 and 240 grit are not interchangeable specifications.
- Approve a physical limit sample.ASTM A480 appearance varies by producer.
- Keep weld repair in the same grain direction.Cross-grain blending remains visible.
Brushed versus the alternatives
Finishes engineers weigh against Brushed, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
Brushed this page | 5 | — | 75 | $$ | 0 µm | — |
| 8 | — | 82 | $$$ | 0 µm | when a non-directional glossy surface is required | |
| 5 | — | 65 | $ | 0 µm | when a non-directional matte finish is preferred |
The radar overlays Brushed with Polishing, its most common alternative — chosen when a non-directional glossy surface is required. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Brushed Finish is a standard-cost finish ($$): cheaper than about 71 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates cross-checked against US job-shop pricing. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 1–4 working days |
|---|---|
| RoHS | Compliant |
| Notes | Collect metal and abrasive dust; use dedicated abrasives to avoid ferrous contamination of stainless. |
What Brushed is used for
- Stainless appliance panels
- Aluminum faceplates
- Architectural trim
- Elevator interiors
Brushed — frequently asked
brushed vs polished stainless
Brushed stainless has visible directional lines and commonly falls around Ra 0.2–1.6 µm (8–63 µin). Polished stainless uses progressively finer abrasive and can reach Ra 0.1–0.8 µm (4–32 µin) or below.
what is stainless No. 4 finish
No. 4 is a general-purpose directional polished finish identified in ASTM A480/A480M. It is often produced near 180–320 grit, but a sample and Ra limit are needed for a reproducible cosmetic result.
what is No. 8 stainless finish
No. 8 is a highly reflective mirror finish produced by progressive polishing and buffing, not one ordinary brushing pass. Surface acceptance is primarily visual unless the drawing adds an Ra requirement.
what is hairline brushed finish
Hairline is a fine, long, continuous directional grain used on architectural stainless and aluminum. The term has no single universal Ra, so specify grit, direction, and an approved sample.
what grit gives a brushed finish
Abrasive belts from 180–320 grit are common for satin brushing. Alloy, belt condition, pressure, and feed speed can make the same grit look different.
Other mechanical finishing finishes
 Aluminum Bright DipBright dipping is a chemical polishing pretreatment that levels microscopic peaks on aluminum to produce a reflective surface before anodizing.CorrosionHardnessCost$$
 As MachinedAs machined is the baseline CNC condition with no secondary cosmetic finishing.CorrosionHardnessCost$
 DeburringDeburring removes loose or sharp burrs left by cutting, punching, molding, or casting.CorrosionHardnessCost$
 Edge RoundingEdge rounding deliberately replaces a sharp edge with a controlled radius or broad edge break.CorrosionHardnessCost$
 HoningHoning precision-finishes bores with expanding abrasive stones and a controlled cross-hatch.CorrosionHardnessCost$$$
 LappingLapping is a precision loose-abrasive process used to improve flatness, parallelism, and very fine roughness.CorrosionHardnessCost$$$$
 Mirror PolishingMirror polishing removes visible directional scratches and buffs the surface to high specular reflectance.CorrosionHardnessCost$$$$
 Sand BlastingSand blasting uses angular abrasive to remove scale, rust, and coatings or to create a rough coating-ready surface.CorrosionHardnessCost$