
Deburring
Mechanical finishing · Mechanical
Deburring removes loose or sharp burrs left by cutting, punching, molding, or casting.
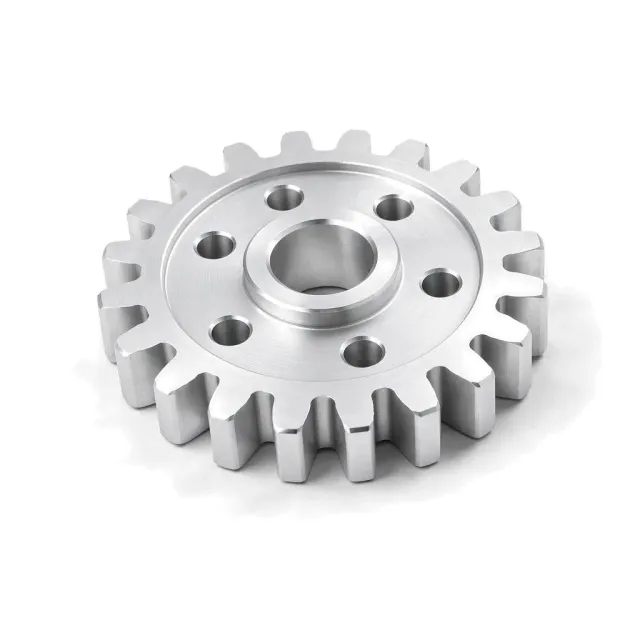
What is Deburr?
It is an edge-condition operation rather than a uniform finish, and the drawing should define the permitted edge break.
How it works
A file, scraper, 120–320 grit abrasive wheel, brush, knife, or controlled mass-finishing cycle cuts or folds away protruding material. The surrounding parent surface should remain untouched unless blending is specified. Mechanically blended edge zones commonly measure Ra 0.8–6.3 µm (32–250 µin), while untouched faces retain their incoming roughness. Inspection focuses on burr-free condition, edge break, and functional fit. Functional Ra is measured under ASME B46.1 or ISO 21920.
Why specify it
- Removes handling hazards
- Prevents assembly interference
- Reduces loose-particle risk
- Can hold a defined 0.1–0.5 mm edge break
Where it falls short
- Does not define a cosmetic all-over finish
- Overwork rounds dimensions and sealing edges
- Internal intersecting-hole burrs are difficult to inspect
- Plastic trimming can leave stress whitening
Deburr at a glance
Deburr is a middle-of-the-range finish; its best score is cosmetic quality (20 of 100), at a budget cost. It adds little corrosion protection or lubricity. Surface hardness is not rated: the finish leaves the part's own surface.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
Deburr key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among mechanical finishing finishes.
- Thickness
- No coating; local blended zones typically Ra 0.8–6.3 µm (32–250 µin), with parent faces unchanged.
- Electrical
- Unchanged
- Appearance
- Burr-free edges with local blend marks; parent surfaces normally unchanged.
Specifications for Deburr
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard.
Drawing call-out
REMOVE ALL BURRS AND LOOSE MATERIAL; BREAK SHARP EDGES 0.2–0.4 mm UNLESS OTHERWISE SPECIFIED; DO NOT BREAK DATUM A EDGESWhich materials take Deburr?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Easy to deburr but also easy to over-round. | |
| Yes | Suitable; protect against smear and media embedment. | |
| Yes | Suitable; expect faster cutting and easier smearing than steel. | |
| Yes | Knife or cryogenic methods may be used; avoid whitening and melt smear. | |
| Yes | Work-hardening burrs may require sharp dedicated tooling. | |
| Yes | Tool selection depends on hardness and burr root. | |
| Yes | Suitable with contamination-controlled tooling or media. | |
| With care | Possible with non-sparking media and fire-safe dust control. | |
| With care | Soft die-cast zinc cuts quickly and can embed media. |
How Deburr is applied, and what it does to the part
- 1Identify burr direction and access
- 2Protect functional edges
- 3Remove burr with selected tool
- 4Blend only if specified
- 5Inspect by sight touch and magnification as required
| Dimensions | Control edge break explicitly; an undefined 'remove sharp edges' note can cause excessive rounding and loss of feature size. |
|---|---|
| Build-up per side | 0 µm — No buildup; local material is removed only at burrs and specified edge breaks. |
| Masking | Rarely needed. Use work instructions or fixtures to protect sealing lands, sharp datums, and intentionally sharp cutting edges. |
| Electrical | Unchanged |
| Appearance | Burr-free edges with local blend marks; parent surfaces normally unchanged. |
| Added lead time | 0–2 working days on top of the bare part |
Design rules for Deburr
What to decide on the drawing before the part goes to the finisher.
- Give an edge-break range.A burr-free note alone does not limit rounding.
- Identify edges that must stay sharp.Datums and cutting edges may be functional.
- Call out internal burr inspection.Intersecting holes are not visible externally.
- Keep cosmetic blending separate.Deburring does not imply all-over polishing.
Deburr versus the alternatives
Finishes engineers weigh against Deburr, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
Deburr this page | 0 | — | 20 | $ | 0 µm | — |
| 0 | — | 35 | $ | 0 µm | when a repeatable radius rather than simple burr removal is required | |
| 5 | — | 50 | $ | 0 µm | when many small parts can be processed together |
The radar overlays Deburr with Edge Rounding, its most common alternative — chosen when a repeatable radius rather than simple burr removal is required. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Deburring is a budget-cost finish ($): cheaper than about 96 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 0–2 working days |
|---|---|
| RoHS | Compliant |
| Notes | Collect chips, abrasive dust, and trimmed polymer separately. |
What Deburr is used for
- Machined blocks
- Laser-cut sheet
- Molded housings
- Cross-drilled manifolds
Deburr — frequently asked
what does deburr and break sharp edges mean
It requires removal of loose burrs plus a controlled edge break. A useful drawing adds a range such as 0.2–0.4 mm and excludes datums or functional sharp edges.
does deburring change dimensions
It should only change the local burr and edge, but over-deburring reduces feature size and rounds corners. Critical edges need explicit limits.
what Ra does deburring produce
Mechanically blended edge zones often fall around Ra 0.8–6.3 µm (32–250 µin). Parent faces should retain their incoming Ra unless blending is requested.
how are cross-hole burrs removed
Common methods include abrasive filaments, shaped cutters, flow finishing, or manual tools. Access and inspection should be planned on the drawing or process sheet.
deburring vs edge rounding
Deburring removes unwanted protrusions. Edge rounding deliberately creates a controlled radius or chamfer and therefore changes the nominal geometry more predictably.
Other mechanical finishing finishes
 Aluminum Bright DipBright dipping is a chemical polishing pretreatment that levels microscopic peaks on aluminum to produce a reflective surface before anodizing.CorrosionHardnessCost$$
 As MachinedAs machined is the baseline CNC condition with no secondary cosmetic finishing.CorrosionHardnessCost$
 Bead BlastingBead blasting propels spherical media at a surface to make a uniform satin or matte finish.CorrosionHardnessCost$
 Brushed FinishBrushing creates a directional grain with abrasive belts, wheels, or pads.CorrosionHardnessCost$$
 HoningHoning precision-finishes bores with expanding abrasive stones and a controlled cross-hatch.CorrosionHardnessCost$$$
 LappingLapping is a precision loose-abrasive process used to improve flatness, parallelism, and very fine roughness.CorrosionHardnessCost$$$$
 Mirror PolishingMirror polishing removes visible directional scratches and buffs the surface to high specular reflectance.CorrosionHardnessCost$$$$
 PolishingMechanical polishing progressively removes surface peaks and scratches to produce a smooth glossy surface.CorrosionHardnessCost$$$