
HP 3D High Reusability PA 11 (PA11, MJF)
HP · MJF powder
A ductile bio-based PA 11 for impact-resistant functional parts, living hinges, and flexible production geometries.
HP datasheet values, printed parts
Other PA11 grades and fills
Compare the PA11 products and conditions in the library; see the grade overview at PA11.
- COND
- FR
- ESD
- GF
- Arkema Rilsan Invent Natural
- EOS PA 1102 black
- EOS PA 1101 ClimateNeutral
- Formlabs Nylon 11
- EOS PA 1101
- Forward AM Ultrasint PA11
- HP PA 11
- HP PA 11 Gen2
- Sinterit PA11 Onyx
- CF
- Formlabs Nylon 11 CF
- Sinterit PA11 CF
- Forward AM Ultrasint PA11 Black CF
Compare all 17 grades and fillsHide
| Grade · open for datasheet | Best for | Yield MPa | Tensile MPa | Elong. % | Hardness |
|---|---|---|---|---|---|
Conditioned | PA11 moisture-conditioned to equilibrium at 50% RH: water plasticizes the amide phase, lowering modulus and strength while raising ductility and impact toughness. | 36 | 45 | 120 | 72 Shore D |
Flame-retardant PA11 powder | Specify for aircraft interior, rail and electrical enclosure parts needing V-0 / FAR 25.853 compliance. | 36 | 40 | 15 | 76 Shore D |
Static-dissipative / conductive-filled PA11 powder | For electronics handling trays, fuel-system components and fixtures requiring controlled surface resistivity. | 38 | 44 | 15 | 77 Shore D |
Glass-bead / glass-fiber filled PA11 powder | Use when stiffness, dimensional stability and elevated-temperature rigidity matter more than ductility. | — | 42 | 6 | 82 Shore D |
SLS powder | — | — | 45 | 45 | 77 Shore D |
SLS powder | — | — | 48 | 30 | — |
SLS powder | — | — | 48 | 45 | — |
Formlabs Nylon 11 Powder · SLS powder | A bio-based, highly ductile PA11 powder for flexible, impact-resistant functional and medical parts. | — | 49 | 40 | — |
SLS powder | — | — | 50 | 30 | 75 Shore D |
SLS powder | — | — | 52 | 28 | — |
HP PA 11This page HP 3D High Reusability PA 11 · MJF powder | A ductile bio-based PA 11 for impact-resistant functional parts, living hinges, and flexible production geometries. | — | 52 | 50 | 80 Shore D |
HP 3D High Reusability PA 11 Gen2 · MJF powder | A second-generation ductile bio-based PA 11 for repeatable final-use production with improved powder efficiency. | — | 52 | 35 | — |
SLS powder | — | — | 55 | 31.6 | 76 Shore D |
Carbon-fiber reinforced PA11 powder | Highest stiffness-to-weight printed PA11; for jigs, brackets and motorsport parts where deflection must be minimized. | 60 | 65 | 5 | 82 Shore D |
Formlabs Nylon 11 CF Powder · SLS powder | A carbon-fiber-filled PA11 powder for strong, lightweight, impact-resistant parts that remain stable at elevated temperatures. | — | 69 | 9 | — |
SLS powder | — | — | 81 | 24.5 | 81 Shore D |
SLS powder | — | — | 82 | 7 | — |
What is HP 3D High Reusability PA 11?
HP 3D High Reusability PA 11 is HP's PA11 powder for Multi Jet Fusion on HP Jet Fusion 5200, 5000 and 4200 series — a ductile bio-based PA 11 for impact-resistant functional parts, living hinges, and flexible production geometries. HP 3D High Reusability PA 11 has a tensile strength of 52 MPa (7.54 ksi), stronger than 56% of polymer grades. Elongation at break is 50% and the elastic modulus is 1.8 GPa (0.261 Msi). HP 3D High Reusability PA 11 has a density of 1.05 g/cm³ (0.0379 lb/in³), lighter than 69% of polymer grades. Pick HP in the Powder row when quoting PA11 and the part is printed from this powder.
About this powder
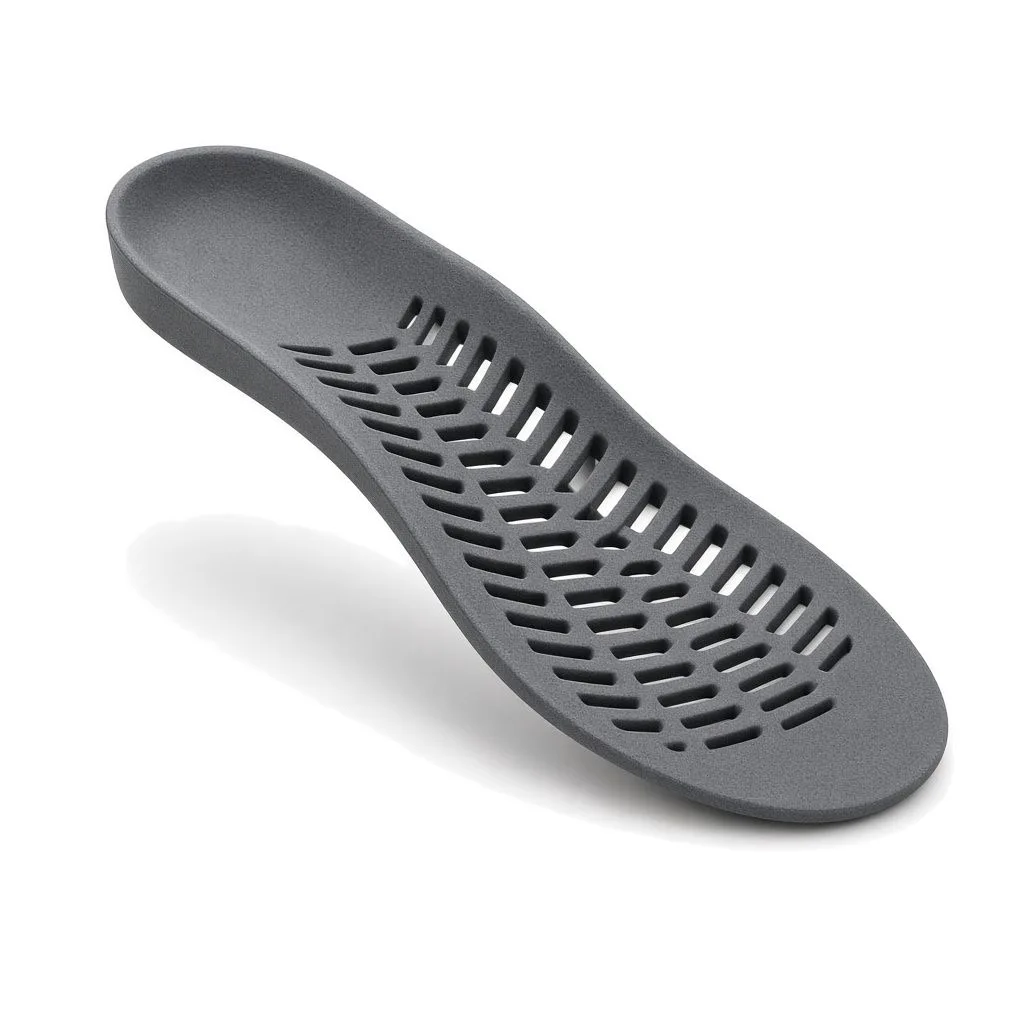
“Ideal for producing strong, ductile functional parts and minimize waste with a quality bio-based material. Engineered for HP MJF and parts that reduce your carbon footprint.” — HP, product description
- Manufacturer
- HP
- Product
- 3D High Reusability PA 11
- Base polymer
- PA11
- Process
- Multi Jet Fusion (MJF)
- Printers
- HP Jet Fusion 5200, 5000 and 4200 series
- As-printed colour
- Gray; dyeing options depend on the base colour and grade
- Build envelope
- 380 × 284 × 380 mm. Usable part size depends on orientation, spacing and process allowances.
- Build atmosphere
- No mandatory inert atmosphere recorded; follow the selected printer/material profile.
- Powder refresh
- 30 % fresh powder in the recorded recipe. Follow the manufacturer’s build and powder-management conditions.
- Reported material classifications
- USP Class I-VI · U.S. FDA guidance for Intact Skin Surface Devices · FMVSS 302. Scope and test conditions apply; these do not certify the finished part or assembly.
- Manufacturer data source
- HP source reference (HP materials page, 2026)
- FabDigit material reference
- Download reference PDF — FabDigit layout with HP data and source attribution.
- Ordering
- Select it in the Powder row when quoting PA11. The quote confirms the selected material and process.
HP positions it for prostheses and orthotics, insoles, sporting goods, snap fits, living hinges and functional and final parts across industries.
Choosing 3D High Reusability PA 11
First-generation HP MJF PA11 for ductile parts, snaps and impact-prone geometry on the Jet Fusion 5200 workflow.
- Consider it for
- Snap features and compliant parts · Orthotic and impact-prone components · Detailed functional parts that need more give than PA12
- Tradeoffs
- HP's current portfolio now distinguishes this 5200 material from PA11 Gen2 on the 5600. Do not transfer Gen2 reuse, cost or sustainability claims to this product.
- Design and validation
- Use the exact printer generation in the drawing and qualification plan. Prototype cyclic flexing and impact geometry in the expected conditioned state.
- Finishing
- Gray is the as-printed colour. Treat dyeing as a separate operation and verify that the chosen finish does not compromise a flexible feature or contact requirement.
- Before choosing
- Is the available route the 5200 material or PA11 Gen2 on the 5600? Does the application need PA11 compliance rather than a stiffer PA12?
Selection notes based on HP MJF materials portfolio. Published test results depend on the stated printer, orientation and conditioning. Compare material families · Choose a finishing route.
HP 3D High Reusability PA 11 properties
Typical values for HP 3D High Reusability PA 11 (HP materials page, 2026); review each property’s test condition. Only this product’s reported properties are shown; unreported properties are omitted. Bars are the position among polymer grades.
Physical2
HP 3D High Reusability PA 11 has a density of 1.05 g/cm³ (0.0379 lb/in³), lighter than 69% of polymer grades.
per ASTM D792
per ASTM D3418; Powder melting point (DSC)
Mechanical7
HP 3D High Reusability PA 11 has a tensile strength of 52 MPa (7.54 ksi), stronger than 56% of polymer grades. Elongation at break is 50% and the elastic modulus is 1.8 GPa (0.261 Msi).
per ASTM D638; XY/XZ/YX/YZ 52 / ZX/ZY 52
per ASTM D638; XY/XZ/YX/YZ 1.8 / ZX/ZY 1.8 GPa
per ASTM D638; XY/XZ/YX/YZ 50 / ZX/ZY 35
per ASTM D790; All orientations 70
per ASTM D790; All orientations 1.8 GPa
per ASTM D256; Izod notched, kJ/m²; XY/XZ/YX/YZ 5 / ZX/ZY 4.5
per ASTM D2240; All orientations 80
Thermal2
per ASTM D648; All orientations 185
per ASTM D648; All orientations 54
Manufacturability2
per ASTM D3451
per ASTM D1895
Use published values for design screening. Confirm the grade, build direction, conditioning and available lot documentation when quoting.
HP 3D High Reusability PA 11 — frequently asked
What is HP 3D High Reusability PA 11 used for?
First-generation HP MJF PA11 for ductile parts, snaps and impact-prone geometry on the Jet Fusion 5200 workflow. Consider it for snap features and compliant parts, orthotic and impact-prone components and detailed functional parts that need more give than PA12. HP's current portfolio now distinguishes this 5200 material from PA11 Gen2 on the 5600. Do not transfer Gen2 reuse, cost or sustainability claims to this product.
What should I validate before using HP 3D High Reusability PA 11?
Use the exact printer generation in the drawing and qualification plan. Prototype cyclic flexing and impact geometry in the expected conditioned state. Is the available route the 5200 material or PA11 Gen2 on the 5600? Does the application need PA11 compliance rather than a stiffer PA12?
How can HP 3D High Reusability PA 11 be finished?
Gray is the as-printed colour. Treat dyeing as a separate operation and verify that the chosen finish does not compromise a flexible feature or contact requirement.
Sources
Product values come from the selected manufacturer source and are normalised for comparison. Confirm the quoted process, build direction, conditioning and available lot documentation for the finished part.