
Steel Stamp Part Marking
Marking & decoration · Mechanical
Steel stamp marking indents characters or symbols with a hardened hand stamp, press die, or roll marker.
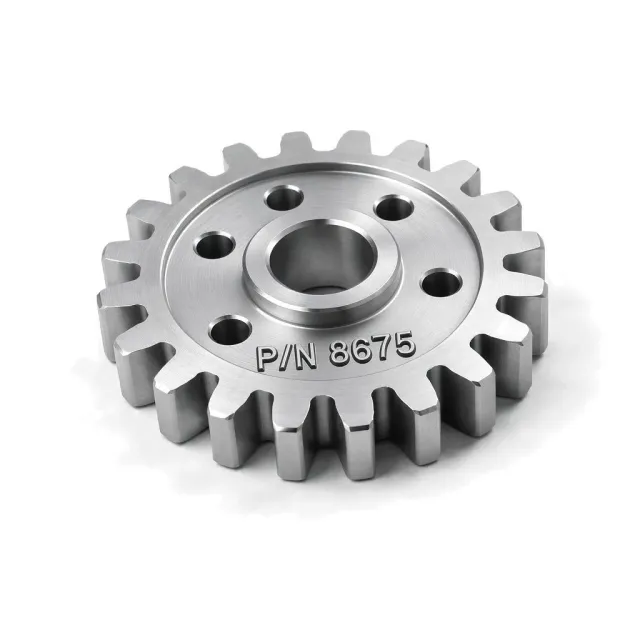
What is Steel stamp?
It creates rugged part numbers, heat codes, and regulatory identification on metal parts.
How it works
A hardened steel character or logo die is aligned over a rigidly supported workpiece and driven by hammer, pneumatic impact, arbor press, or production press. Plastic deformation displaces substrate around the die face and leaves a recessed image. Force, die sharpness, substrate hardness, support, and stroke determine depth and legibility. Fixed gang stamps improve alignment; roll marking reduces peak force on cylindrical parts.
Why specify it
- Creates a permanent indented mark without ink
- Typical identification depth is 100–500 µm
- Low consumable cost for repeated fixed characters
- Readable after paint loss or surface contamination
Where it falls short
- Impact can distort thin walls and cosmetic surfaces
- Hard or brittle materials may crack or damage stamps
- Character changes are manual unless automated
- Indentations are stress concentrators
Steel stamp at a glance
Steel stamp is a middle-of-the-range finish; its best score is cosmetic quality (38 of 100), at a budget cost. It adds little corrosion protection or lubricity. Surface hardness is not rated: the finish leaves the part's own surface.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
Steel stamp key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among marking & decoration finishes.
- Thickness
- 100–500 µm indentation depth for metal part identification; depth depends on hardness and support.
- Electrical
- Unchanged
- Colours
- substrate colour
- Appearance
- Indented block characters or symbols with displaced edges and an industrial appearance.
Specifications for Steel stamp
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard, and US Government documents are free to download there.
Test and related methods: MIL-STD-130 (Identification Marking of U.S. Military Property).
Drawing call-out
STEEL-DIE STAMP PART NO. AND HEAT CODE PER MIL-STD-130, 3 MM CHARACTER HEIGHT, 0.20–0.30 MM DEEP; LOCATE AS SHOWNWhich materials take Steel stamp?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Marks readily but thin walls deform. | |
| Yes | Takes a clear indent at moderate force. | |
| Yes | Common when hardness and section support permit. | |
| With care | Soft copper takes a deep indent and can bulge the reverse face. | |
| With care | Impact can crack thin magnesium; laser marking is preferred. | |
| With care | Higher force may be required; avoid fatigue-critical areas. | |
| With care | Soft zinc takes a clear indent at low force but can bulge the reverse face. | |
| Limited | Hard titanium can crack stamps or the part; laser marking is preferred. | |
| No | Impact character stamps do not produce a durable mark in most polymers. |
How Steel stamp is applied, and what it does to the part
- 1Select and arrange stamp
- 2Support part
- 3Align to datum
- 4Apply controlled impact or press force
- 5Inspect content, depth, and deformation
| Dimensions | The 100–500 µm indentation displaces material and may bulge the opposite face of thin sections. |
|---|---|
| Masking | Rarely needed. Protect adjacent finished surfaces and fixture contact areas from impact damage. |
| Electrical | Unchanged |
| Appearance | Indented block characters or symbols with displaced edges and an industrial appearance. |
| Added lead time | 1–2 working days on top of the bare part |
Design rules for Steel stamp
What to decide on the drawing before the part goes to the finisher.
- Provide solid backing directly beneath the mark.Unsupported walls bend instead of taking a clean impression.
- Keep marking away from edges, bends, and fatigue-critical zones.Impact deformation and notches concentrate stress.
- Specify character height, depth, orientation, and location.A generic 'stamp part' note is not inspectable.
- Verify substrate hardness against die capability.Hard parts can chip dies or produce incomplete marks.
Steel stamp versus the alternatives
Finishes engineers weigh against Steel stamp, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
Steel stamp this page | 0 | — | 38 | $ | 100–500 µm | — |
| 0 | — | 35 | $ | 50–500 µm | for automated variable characters | |
| 0 | — | 70 | $ | 0–50 µm | when deformation is unacceptable |
The radar overlays Steel stamp with Dot Peen Marking, its most common alternative — chosen for automated variable characters. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Steel Stamp Part Marking is a budget-cost finish ($): cheaper than about 90 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 1–2 working days |
|---|---|
| RoHS | Compliant |
| Notes | The operation adds no material; lubricant or paint fill, if used, requires separate compliance review. |
What Steel stamp is used for
- Heat codes
- Part numbers
- Forging identification
- Fabricated brackets
- Heavy-equipment components
Steel stamp — frequently asked
Steel stamping vs dot peen marking: what is the difference?
A steel stamp forms each character with a shaped die and commonly indents 100–500 µm in one impact. Dot peen builds characters from many small impacts and is easier to automate for variable serial data.
How deep should stamped part numbers be?
Use 100–500 µm as a typical metal identification range, then limit it for wall thickness and stress. The drawing should give a measurable minimum and maximum.
Can you stamp hardened steel parts?
Only if the stamp and machine are rated for the part hardness. Laser or electrochemical marking is often safer because impact stamping can chip tools or crack a hard part.
Does steel stamp marking weaken a part?
The indentation is a notch and the impact plastically deforms material. Keep it away from highly stressed edges and thin walls, and obtain engineering approval for fatigue-critical parts.
Can steel stamps mark aluminum and titanium?
Yes, with force and die geometry adjusted to the alloy and section. Soft aluminum deforms readily, while titanium needs stronger support and process trials.
Other marking & decoration finishes
 Chemical EtchingChemical etching uses a patterned resist and material-specific etchant to recess graphics or create a frosted contrast.CorrosionHardnessCost$$$
 Electrochemical EtchingElectrochemical etching makes a localized permanent mark on an electrically conductive part through a stencil and electrolyte.CorrosionHardnessCost$$
 Embossing and DebossingEmbossing raises artwork above a surface, while debossing recesses it through forming dies or molded tool geometry.CorrosionHardnessCost$$$
 Hot StampingHot stamping uses a heated die to transfer pigmented or metallic foil onto a part.CorrosionHardnessCost$$
 In-Mold Decoration (IMD)In-mold decoration places a formed, printed decorative film in an injection mold so the graphic becomes part of the molded surface.CorrosionHardnessCost$$$$
 In-Mold Labeling (IML)In-mold labeling places a preprinted label in the mold before plastic is injected.CorrosionHardnessCost$$$
 Ink StampingInk stamping transfers a fixed image from a rubber, polymer, or metal stamp onto a part.CorrosionHardnessCost$
 Mechanical EngravingMechanical engraving cuts text, symbols, serials, or decorative lines into a surface with a rotating or dragging tool.CorrosionHardnessCost$$