
Ink Stamping
Marking & decoration · Printing
Ink stamping transfers a fixed image from a rubber, polymer, or metal stamp onto a part.
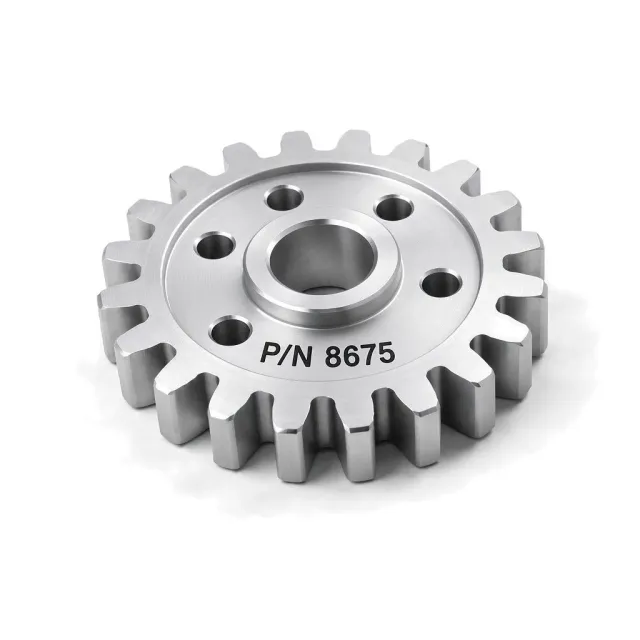
What is Ink stamp?
It is a fast low-cost method for inspection marks, lot codes, simple logos, and noncritical regulatory text.
How it works
A relief stamp is inked from a pad or roller, aligned to the part, and pressed against the surface. Raised features transfer a thin wet film that then dries or cures. Hand stamps suit low volume; fixtures and roll coders improve position and repeatability. Ink chemistry, stamp hardness, contact pressure, dwell, substrate cleanliness, and surface energy determine image completeness and adhesion.
Why specify it
- Lowest setup for simple repeated fixed marks
- Typical cured film is about 3–8 µm
- Fast for inspection and lot-control marks
- Supports multiple ink colours with separate operations
Where it falls short
- Lower detail and registration than pad or screen printing
- Hand stamping varies in density and position
- Fixed stamps are inefficient for frequently changing data
- Ink wears or dissolves unless specifically qualified
Ink stamp at a glance
Ink stamp is a middle-of-the-range finish; its best score is cosmetic quality (35 of 100), at a budget cost. It adds little corrosion protection or lubricity. Surface hardness is not rated: the finish leaves the part's own surface.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
Ink stamp key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among marking & decoration finishes.
- Thickness
- 3–8 µm cured ink film; thickness is deposited film and varies with stamp loading.
- Electrical
- Unchanged
- Colours
- black
- white
- red
- blue
- custom ink
- Appearance
- Simple thin-film mark with moderate edge definition and possible density variation.
Specifications for Ink stamp
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard.
| Standard | Type / Class | Thickness | Requirement / test | Status |
|---|---|---|---|---|
Paints and Varnishes — Cross-Cut Test · ISO · alternative | Classification 0 | — | Cut edges completely smooth; no lattice squares detached · Visual comparison after cross-cut procedure | Active |
| Classification 1 | — | Small flakes detached at intersections; affected area not significantly greater than 5% · Visual comparison after cross-cut procedure | ||
| Classification 2 | — | Flaking along edges or intersections affecting more than 5% but not significantly more than 15% · Visual comparison after cross-cut procedure | ||
| Classification 3 | — | Flaking in ribbons or parts of squares affecting more than 15% but not significantly more than 35% · Visual comparison after cross-cut procedure | ||
| Classification 4 | — | Large ribbons or squares detached, affecting more than 35% but not significantly more than 65% · Visual comparison after cross-cut procedure | ||
| Classification 5 | — | Flaking greater than classification 4 · Visual comparison after cross-cut procedure |
Test and related methods: ASTM D3359 (Standard Test Methods for Rating Adhesion by Tape Test).
Drawing call-out
INK STAMP INSPECTION CODE, BLACK, 3 MM CHARACTER HEIGHT, LOCATION ±1.0 MM; ASTM D3359 CLASS 4B MIN AFTER FULL CUREPattern: CROSS-CUT ADHESION PER ISO 2409, MAXIMUM CLASSIFICATION <0–5>
Which materials take Ink stamp?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Common on clean coated or anodized surfaces. | |
| Yes | Common on clean paint, plating, or bare metal with suitable ink. | |
| With care | Tarnish reduces ink adhesion; clean immediately before stamping. | |
| With care | Ink adhesion on copper needs a clean, tarnish-free surface and a qualified ink. | |
| With care | Use glass-compatible ink and cure. | |
| With care | Ink adhesion is poor on reactive magnesium unless conversion-coated or primed. | |
| With care | Resin-specific ink and surface activation may be needed. | |
| With care | Smooth low-energy surfaces require ink validation. | |
| With care | Possible on clean or painted zinc; bare castings often reject ink. | |
| Limited | Bare titanium is a poor ink-stamp surface; laser marking is preferred. |
How Ink stamp is applied, and what it does to the part
- 1Clean surface
- 2Ink stamp
- 3Align or fixture
- 4Press stamp
- 5Dry or cure
- 6Inspect content and adhesion
| Dimensions | Local 3–8 µm buildup is normally negligible except on contacts and tight interfaces. |
|---|---|
| Build-up per side | 3–8 µm — Ink builds locally above the substrate. |
| Masking | Usually needed. Keep ink off contacts, seals, bonding areas, and precision fits. |
| Electrical | Unchanged |
| Appearance | Simple thin-film mark with moderate edge definition and possible density variation. |
| Added lead time | 1–2 working days on top of the bare part |
Design rules for Ink stamp
What to decide on the drawing before the part goes to the finisher.
- Use bold open characters at least 2 mm high for hand stamping.Thin features and small counters fill or print incompletely.
- Provide a flat area larger than the stamp pad.All raised features need simultaneous contact.
- State location tolerance appropriate to manual or fixtured application.Hand stamping cannot hold precision print registration.
- Specify ink family, colour, cure, and permanence test.Generic stamp ink may fail solvent or abrasion exposure.
Ink stamp versus the alternatives
Finishes engineers weigh against Ink stamp, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
Ink stamp this page | 0 | — | 35 | $ | 3–8 µm | — |
| 0 | — | 72 | $ | 5–10 µm | for finer graphics on curved surfaces | |
| 0 | — | 70 | $ | 0–50 µm | for permanent variable serial data |
The radar overlays Ink stamp with Pad Printing, its most common alternative — chosen for finer graphics on curved surfaces. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Ink Stamping is a budget-cost finish ($): cheaper than about 99 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 1–2 working days |
|---|---|
| RoHS | Compliant |
| Notes | Ink pigments, solvents, and curing agents require supplier declarations and controlled handling. |
What Ink stamp is used for
- Inspection acceptance marks
- Lot codes
- Simple logos
- Date codes
- Assembly orientation marks
Ink stamp — frequently asked
Ink stamping vs pad printing: which is better?
Ink stamping is cheaper and faster for simple fixed marks but offers less detail and location control. Pad printing uses a silicone pad, reaches curved surfaces, and typically deposits a controlled 5–10 µm film.
How thick is an ink-stamped mark?
A typical cured film is about 3–8 µm, depending on ink loading and stamp pressure. Treat that as local buildup where contacts or fits are sensitive.
Is ink stamping permanent?
It can survive normal handling when the ink matches the substrate, but it is less permanent than laser, engraving, or dot peen. Qualify adhesion and a defined alcohol-rub or abrasion cycle for the service environment.
Can ink stamping be used on metal and plastic?
Yes, but the same ink rarely performs equally on bare metal, coated metal, and low-surface-energy plastic. Validate each substrate and finish with the production cure.
How do you test ink-stamp adhesion?
ASTM D3359 or ISO 2409 can evaluate adhesion where film and geometry permit. A solvent rub must separately state alcohol concentration, load, stroke length, and cycle count.
Other marking & decoration finishes
 Chemical EtchingChemical etching uses a patterned resist and material-specific etchant to recess graphics or create a frosted contrast.CorrosionHardnessCost$$$
 Dot Peen MarkingDot peen marking uses a controlled stylus to build characters and Data Matrix symbols from small permanent indentations.CorrosionHardnessCost$
 Electrochemical EtchingElectrochemical etching makes a localized permanent mark on an electrically conductive part through a stencil and electrolyte.CorrosionHardnessCost$$
 Embossing and DebossingEmbossing raises artwork above a surface, while debossing recesses it through forming dies or molded tool geometry.CorrosionHardnessCost$$$
 Hot StampingHot stamping uses a heated die to transfer pigmented or metallic foil onto a part.CorrosionHardnessCost$$
 In-Mold Decoration (IMD)In-mold decoration places a formed, printed decorative film in an injection mold so the graphic becomes part of the molded surface.CorrosionHardnessCost$$$$
 In-Mold Labeling (IML)In-mold labeling places a preprinted label in the mold before plastic is injected.CorrosionHardnessCost$$$
 Mechanical EngravingMechanical engraving cuts text, symbols, serials, or decorative lines into a surface with a rotating or dragging tool.CorrosionHardnessCost$$