
5-Axis CNC Machining
Angled ports, compound-angle faces and contoured surfaces machined in one or two setups instead of five. Aluminum, stainless steel and titanium, from one piece, priced from your CAD in minutes.
±0.025 mm
On toleranced features
2 setups
Instead of 5 on the sample housing
500 mm
Longest side, standard envelope
From 1 pc
No minimum order
What we machine
Parts with features on several faces, or surfaces a 3-axis tool cannot reach square-on.
Multi-face housings
Pockets, ports and tapped holes on five faces, all referenced to one datum set in a single fixture.
Manifolds and fluid blocks
Angled, intersecting bores with sealing faces machined square to each port.
Impellers and blades
Simultaneous 5-axis contouring of blended surfaces, no witness lines between setups.
Compound-angle brackets
Mounting faces and hole patterns at non-orthogonal angles, positioned to each other in one clamping.
Optical and sensor mounts
Tilted bores and reference faces where angular position matters more than size.
Fixtures and jigs
Locating faces and dowel holes in several orientations, cut without re-indicating the part.
3-axis, 3+2 or simultaneous 5-axis
Axis count is not a quality grade. It decides how many times the part is re-clamped, and which surfaces the tool can reach.
| Route | Motion | Setups on the sample housing | Geometry it unlocks | Choose it for |
|---|---|---|---|---|
| 3-axisX · Y · Z | Tool moves in three axes; the part is re-fixtured for every face. | 5 setupsone per machined face | Flat faces, pockets and holes normal to one face at a time. | Plates, brackets and simple housings; the lower price at volume. |
| 3+2 indexedX · Y · Z + tilt · rotate | Table tilts and rotates to a fixed angle, then the machine cuts as a 3-axis. | 2 setupstop, then flip | Angled holes and faces; features on five sides from one datum set; short, rigid tools. | Multi-face housings, manifolds, compound-angle brackets. |
| Simultaneous 5-axisall axes move while cutting | The tool tilts continuously to follow the surface. | 1–2 setups | Impellers, blades, blended and undercut surfaces. | Free-form contours and aerospace-style geometry. |
Setup counts are for the sample housing in the cost section (pockets on five faces). Your quote picks the route from the geometry you upload.
Materials
The grades we quote instantly for 5-axis work. Every row links to the datasheet with tempers, heat treatments and finishes.
| Material | Machinability | Cost | Use it for |
|---|---|---|---|
| Aluminum 6061 | Very good | $ | General CNC machined parts; Aerospace and structural brackets; Hydraulic manifolds and valve bodies |
| Aluminum 7075 | Excellent | $$$ | Aerospace components; Defense equipment; Gears |
| Aluminum 2024 | Excellent | $$$ | Aircraft skins and fuselage panels; Wing and fuselage structural members; Aerospace fittings and brackets |
| Stainless Steel 304 | Fair | $$ | Food processing equipment; Kitchen appliances and sinks; Sanitary tanks and process piping |
| Stainless Steel 316 | Fair | $$$ | Marine deck hardware and fasteners; Chemical process piping and tanks; Food and pharmaceutical processing equipment |
| Stainless Steel 17-4 PH | Fair | $$$ | Pump shafts; Valve stems and internals; Aerospace structural fittings |
| Steel 4140 | Good | $$ | CNC machined gears; Transmission and drive shafts; Machine tool spindles |
| Copper Alloy C36000 | Excellent | $$$ | CNC turned threaded parts and fasteners; Hydraulic and pneumatic fittings; Valve stems and valve cores |
| Titanium Grade 5 | Poor | $$$ | Aircraft turbine blades and engine hardware; Medical implants and instrument bodies; Airframe structural fittings and lugs |
| PEEK | Very good | $$$$$ | Spinal fusion implants; Aerospace seals and back-up rings; Downhole oil and gas seals |
Machinability and weldability are the library’s 0–100 scores (Excellent ≥ 85 … Poor < 35); cost is the relative tier, not a price. Every grade links to its datasheet with tempers, heat treatments and the finishes it takes.
5-axis cost against 3-axis
The same housing priced twice: as a 3-axis job with five setups and as a 5-axis job with two. At quantity 1 the 5-axis route costs 30 % less; at quantity 100 the two routes are within 7 % of each other.
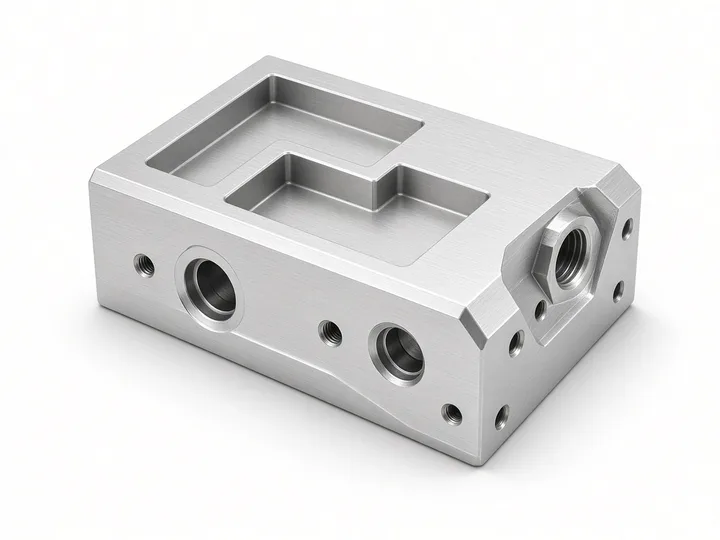
Five-face housing
Aluminum 6061-T6 · 120 × 80 × 40 mm · pockets on five faces · 12 holes, 4 tapped M5 · ±0.05 mm on datum features · as machined
Cost per part by quantity — the same housing on both routes
Aluminum 6061-T6, standard schedule, as machined. 100 % = the 3-axis route at quantity 1. The 5-axis route starts 30 % lower; by quantity 100 the two lines are 7 % apart — setup time is a fixed cost that spreads thin at volume.
| Material | Cost index · 5-axis, qty 1 | 5-axis saving · qty 1 | qty 10 | qty 50 | qty 100 |
|---|---|---|---|---|---|
| Aluminum 6061-T6 | 1.0× | −30 % | −10 % | −6 % | −7 % |
| Aluminum 7075-T6 | 1.4× | −24 % | −8 % | −4 % | −4 % |
| Stainless 304 | 1.2× | −26 % | −8 % | −4 % | −2 % |
| Titanium Grade 5 | 4.4× | −9 % | −2 % | −1 % | −1 % |
Cost index: aluminum 6061 on the 5-axis route at quantity 1 = 1.0×. Saving: 5-axis (2 setups) against 3-axis (5 setups) for the same material and quantity.
Not a quote. Ratios from the FabDigit quote engine, September 2026, for the housing shown, standard schedule, as machined. The saving is setup time: two clampings instead of five. It is largest on one-offs and spreads thin at volume, so above about 50 pieces choose the route by geometry, not by price. Your part gets its own number from the quote. Full method in the CNC machining cost guide.
Tolerances and finishes
What the standard order holds, and what to call out on the drawing.
| Feature | Standard | On the drawing |
|---|---|---|
| Toleranced dimensions | ±0.025 mmtighter grades per feature (ISO 286) | Tolerance the fits, datums and sealing faces; leave the rest general. |
| General tolerance | ISO 2768-mor -f on request | One note covers every untoleranced dimension. |
| Angular position | Held in one setupfeatures on five faces to one datum set | State the datum scheme; angular tolerances on the ports, not the box. |
| Surface roughness | Ra 0.8–1.6 µmas machined; Ra 0.4 µm on request | Call out sealing and bearing faces individually. |
| Minimum feature | 1 × 1 × 5 mmtypical milling minimum | Deep, narrow pockets drive tool length and price. |
| Envelope | 500 × 500 × 500 mmlarger on review | Upload the full assembly if parts must match. |
| Finishes | As machined Bead blast Anodize II / III Passivate Powder coat | Pick the finish in the quote; masked faces and threads are noted there. Finish library. |
When to choose something else
Most machined parts do not need a fourth or fifth axis. These routes are cheaper when they fit the geometry.
How to order
- Upload a STEP file. Pick the material, finish and quantity. Add a PDF drawing and we read the tolerances, threads and datums from it.
- Check the price and DFM notes. The quote shows the standard and expedited ship dates side by side, with flags for thin walls, deep pockets and tool access.
- Order online. Every order is first-article inspected; dimensional or CMM reports and material certificates are available on request.
Questions about 5-axis machining
Can I order a single 5-axis part?
Yes. There is no minimum order. The cost curve above starts at quantity 1, and most 5-axis orders are one to ten pieces.
How much more does 5-axis machining cost than 3-axis?
For the same part it usually costs less, not more, because it removes setups. The sample aluminum housing costs 30 % less as a two-setup 5-axis job than as a five-setup 3-axis job at quantity 1. At quantity 100 the gap closes to about 7 %.
Do I need simultaneous 5-axis or is 3+2 enough?
Most housings, manifolds and brackets only need 3+2 indexing: the table tilts to each angle and the machine cuts as a 3-axis. Simultaneous motion is for blended surfaces such as impeller blades. You do not choose the route; it is set from your geometry.
What tolerance do you hold?
±0.025 mm on dimensions that carry a tolerance, ISO 2768-m on everything else. Because five faces are machined from one datum set, port-to-port angular position is held without stacking setup errors.
Which materials can be machined on 5 axes?
Every grade in the materials table: aluminum 6061, 7075 and 2024, stainless 304, 316 and 17-4 PH, 4140 steel, brass C360, titanium Grade 5 and PEEK. The full CNC material library is quotable, with machinability shown per grade.
How long does a 5-axis order take?
The quote shows two ship dates, standard and expedited, for the exact part and quantity. The expedited schedule adds a premium to the part price; finishing such as anodizing adds working days on either schedule.
Which files should I upload?
A STEP file is enough for a price. Add a PDF drawing when the part has toleranced fits, threads, a datum scheme or a specified finish; the drawing is read automatically and its callouts flow into the quote.
Price your 5-axis part now
STEP file in, price out. Add a drawing and the tolerances, threads and finish are read from it.
Get an instant quote