
Black Oxide
Black oxide & phosphate · Chemical bath
Black oxide converts the surface of ferrous parts to black magnetite for low-reflectance appearance and minimal dimensional change.
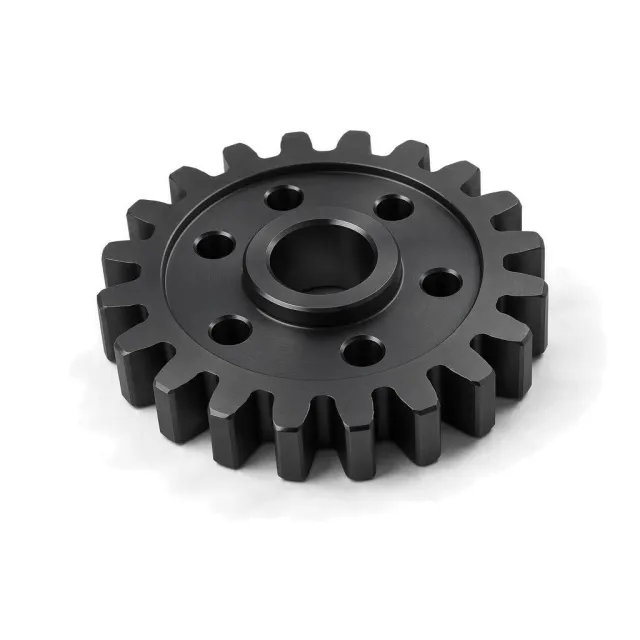
What is Black oxide?
MIL-DTL-13924 covers classes for wrought iron, carbon and low-alloy steel, corrosion-resistant steel, and cast iron.
How it works
Clean ferrous parts are immersed in an alkaline oxidizing salt bath; the common hot process operates near 135–145 °C. The reagent converts surface iron to adherent black magnetite rather than depositing a separate thick layer. The conversion film is commonly about 0.5–2 µm and provides little corrosion protection by itself. Oil, wax, or lacquer fills surface porosity after rinsing and supplies most of the practical rust resistance.
Why specify it
- Only about 0.5–2 µm thick
- Maintains thread and bearing-fit dimensions
- Produces nonreflective black appearance
- Oil or wax gives mild indoor corrosion protection
Where it falls short
- Bare black oxide provides little rust protection
- Not suitable for prolonged outdoor or salt exposure
- After-finish oil can interfere with bonding and cleanliness
- Different MIL-DTL-13924 classes apply to different ferrous alloys
Black oxide at a glance
Black oxide is a middle-of-the-range finish; its best score is cosmetic quality (55 of 100), at a budget cost. Surface hardness is not rated: the finish leaves the part's own surface.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
Black oxide key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among black oxide & phosphate finishes.
- Thickness
- Approximately 0.5–2 µm; practical dimensional change is usually negligible.
- Corrosion (salt spray)
- 24–72 h per ASTM B117 to red rust with supplementary oil or wax (typical) — MIL-DTL-13924 qualifies the coating with an oxalic-acid spot test, not salt spray; unoiled black oxide rusts within hours.
- Electrical
- Semi-conductive
- Colours
- black
- Appearance
- Uniform matte to satin black; final sheen depends on polish and oil, wax, or lacquer.
Specifications for Black oxide
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard, and US Government documents are free to download there.
| Standard | Type / Class | Thickness | Requirement / test | Status |
|---|---|---|---|---|
Coating, Inorganic, Black, for Ferrous Metals · DoD | Class 1 | — | For wrought iron, cast and malleable irons, plain-carbon steel, and low-alloy steel. · Uniform black coverage, smut test, oxalic-acid spot test, and supplementary-finish requirements. | Active |
| Class 2 | — | For specified corrosion-resistant steels tempered below 900 °F (482 °C). · Uniform black coverage, smut test, oxalic-acid spot test, and applicable corrosion test. | ||
| Class 3 | — | For corrosion-resistant steels tempered at 900 °F (482 °C) or above. · Uniform black coverage, smut test, and applicable corrosion test. | ||
| Class 4 | — | For other corrosion-resistant steel alloys. · Uniform black coverage and smut test; 300-series specimens require 96 h salt spray without corrosion before preservative. |
Drawing call-out
BLACK OXIDE PER MIL-DTL-13924 CLASS 1, WITH WATER-DISPLACING PRESERVATIVE OIL; UNIFORM BLACK APPEARANCEPattern: BLACK OXIDE PER MIL-DTL-13924 CLASS <1|2|3|4>, [SUPPLEMENTARY PRESERVATIVE], [MASKING]
Which materials take Black oxide?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Carbon and low-alloy steels are common substrates.
| |
| With care | Steel DMLS/SLM parts may be processed after density and residual-powder review. | |
| With care | Requires a stainless-specific class and chemistry.
| |
| No | Use black anodize or another aluminum finish. | |
| No | Brass does not accept this ferrous conversion coating. | |
| No | Copper alloys do not form this ferrous conversion coating. | |
| No | Fused-filament polymers are incompatible with this process. | |
| No | Magnesium is incompatible with this process. | |
| No | Polymer powder-bed prints are incompatible with this process. | |
| No | Organic polymers cannot take this inorganic metal-finishing process. | |
| No | Photopolymer prints are incompatible with this process. | |
| No | Polymer powder-bed prints are incompatible with this process. | |
| No | Titanium is not processed in these ferrous baths. | |
| No | Zinc alloys are not the intended substrate. |
How Black oxide is applied, and what it does to the part
- 1Clean / degrease
- 2Rinse
- 3Descale / activate
- 4Black oxidize
- 5Oil / wax / lacquer
- 6Drain and dry
| Dimensions | At 0.5–2 µm, black oxide is usually treated as dimensionally negligible for threads and close fits. |
|---|---|
| Build-up per side | 0–0.5 µm — Conversion occurs at the original surface; net dimensional change is normally treated as zero for threads and fits. |
| Masking | Rarely needed. Mask only surfaces that must remain chemically untouched or free of the specified oil/wax after-finish. |
| Electrical | Semi-conductive |
| Temperature limit | 300 °C (572 °F) continuous |
| Appearance | Uniform matte to satin black; final sheen depends on polish and oil, wax, or lacquer. |
| Added lead time | 2–4 working days on top of the bare part |
Design rules for Black oxide
What to decide on the drawing before the part goes to the finisher.
- State the required supplemental oil, wax, or lacquer.The black conversion alone provides little corrosion resistance.
- Select the MIL-DTL-13924 class by alloy.Carbon steel, corrosion-resistant steel, and cast iron use different processing.
- Remove heat-treatment scale before processing.Black oxide will not hide or convert heavy scale uniformly.
- Keep oiled surfaces away from adhesive joints.The corrosion-protective after-finish reduces adhesion.
Black oxide versus the alternatives
Finishes engineers weigh against Black oxide, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
Black oxide this page | 38 | — | 55 | $ | 0.5–2 µm | — |
| 38 | — | 25 | $$ | 5–20 µm | when greater oil retention and break-in wear performance are required | |
| 38 | — | 18 | $ | 2–15 µm | when the primary purpose is a paint base |
The radar overlays Black oxide with Manganese Phosphate, its most common alternative — chosen when greater oil retention and break-in wear performance are required. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Black Oxide is a budget-cost finish ($): cheaper than about 94 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates cross-checked against US job-shop pricing. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 2–4 working days |
|---|---|
| RoHS | Compliant |
| Notes | Typical black oxide can be RoHS compliant; verify supplemental oil, seal, and bath chemistry. |
What Black oxide is used for
- Hand tools
- Precision steel fasteners
- Machine components
- Low-reflectance optical hardware
Black oxide — frequently asked
Does black oxide prevent rust?
Only mildly, and mainly because of the oil, wax, or lacquer after-finish. The 0.5–2 µm magnetite conversion alone is not appropriate for sustained outdoor or salt exposure.
Does black oxide add thickness?
Dimensional change is normally negligible. The converted layer is commonly about 0.5–2 µm, so precision threads are often processed without masking.
Is black oxide conductive?
Magnetite is semiconductive and the thin finish can preserve practical continuity. Contact resistance depends strongly on oil, cleanliness, pressure, and substrate, so critical grounds require testing.
Can stainless steel be black oxidized?
Yes, using a process intended for corrosion-resistant steel, such as the applicable MIL-DTL-13924 class. It is not the same bath control used for ordinary carbon steel.
Black oxide vs phosphate: which should I use?
Choose black oxide for minimal buildup and black appearance. Choose manganese phosphate for oil retention and break-in wear, or zinc phosphate as a paint pretreatment.