
Stainless Steel Passivation
Passivation & electropolishing · Chemical bath
Passivation removes free iron and shop contamination from stainless steel so its chromium-rich passive film can reform.
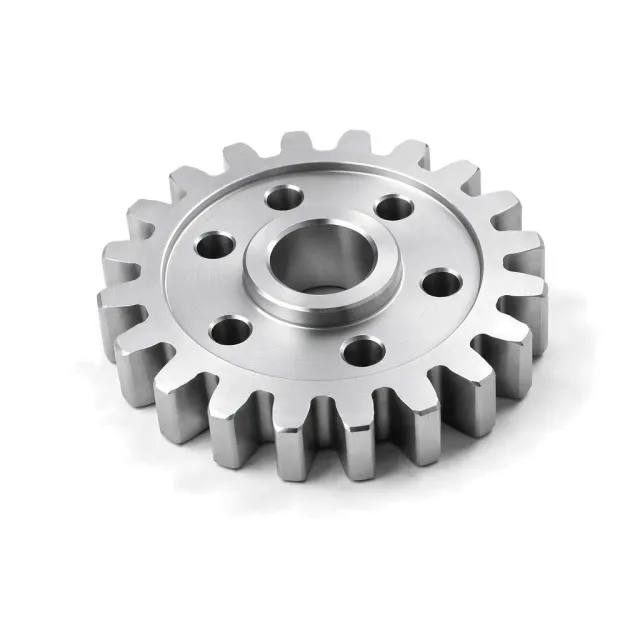
What is Stainless passivation?
ASTM A967 and AMS 2700 define nitric and citric-acid routes plus verification tests for medical, food, aerospace, and general engineering parts.
How it works
After alkaline cleaning, parts are immersed in a controlled nitric-acid or citric-acid solution. The treatment preferentially dissolves free iron and iron-rich contamination without intentionally removing significant stainless substrate. Rinsing and exposure to oxygen allow the nanometer-scale chromium-rich oxide film to reform. Nitric methods have the longest aerospace history; citric methods avoid nitric fumes and are effective when chemistry, temperature, and time are qualified. Acceptance uses water immersion, high humidity, salt spray, copper sulfate, or ferroxyl testing as allowed by the governing specification.
Why specify it
- Removes embedded free iron that can rust
- Adds no measurable coating thickness
- ASTM A967 and AMS 2700 offer nitric and citric methods
- Preserves dimensions of precision and AM parts
Where it falls short
- Does not remove heavy weld scale; pickle first
- Does not repair heat tint depleted of subsurface chromium
- Does not make an unsuitable stainless grade immune to chlorides
- Carbon-steel tooling can recontaminate the surface
Stainless passivation at a glance
Stainless passivation is a middle-of-the-range finish; its best score is corrosion protection (34 of 100), at a budget cost. It adds little lubricity. Surface hardness is not rated: the finish leaves the part's own surface.
Each score is 0–100 against every finish in this catalog. Corrosion comes from salt-spray life (ASTM B117, log scale) and hardness from the finish layer's Vickers or pencil hardness; cosmetic, lubricity and cost are FabDigit's engineering assessment. Economy on the radar is the inverse of cost.
Stainless passivation key numbers
Typical values from the governing specifications and shop practice; bars are this finish against the highest value among passivation & electropolishing finishes.
- Thickness
- 0 µm (0 mil) — No measurable deposited coating; the natural passive film is nanometer-scale.
- Electrical
- Unchanged
- Appearance
- Normally no visible change on a properly cleaned stainless surface.
Specifications for Stainless passivation
The documents a drawing cites to define this finish, with the Type / Class rows that apply. Each links to a page explaining the standard.
| Standard | Type / Class | Thickness | Requirement / test | Status |
|---|---|---|---|---|
Standard Specification for Chemical Passivation Treatments for Stainless Steel Parts · ASTM | Nitric 1–5 | — | Five nitric-acid treatment windows differing in concentration, temperature, time, and optional oxidizing salt · One or more specified passivation verification tests | Active |
| Citric 1–5 | — | Five citric-acid treatment windows differing in concentration, temperature, and time · One or more specified passivation verification tests | ||
Passivation of Corrosion Resistant Steels · SAE · alternative | Method 2 | — | Citric-acid passivation using 4–10% anhydrous citric acid with time selected by bath temperature. · Specified acceptance-class corrosion test and water-break-free cleanliness. | Active |
Test and related methods: ASTM A380 (Standard Practice for Cleaning, Descaling, and Passivation of Stainless Steel Parts, Equipment, and Systems).
Drawing call-out
PASSIVATE PER ASTM A967, NITRIC 2, OR AMS 2700 METHOD 1; VERIFY BY WATER IMMERSION TEST; NO VISIBLE ETCHING OR DISCOLORATIONPattern: PASSIVATE PER ASTM A967, <NITRIC|CITRIC> <1–5>, TEST <METHOD>
Which materials take Stainless passivation?
Verdict per material family, with the grades that behave differently. Each family links to its datasheets in the material library.
| Material family | Verdict | Notes |
|---|---|---|
| Yes | Austenitic, ferritic, martensitic, precipitation-hardening, and AM stainless grades require grade-appropriate cycles.
| |
| With care | Applicable to stainless DMLS/SLM after complete depowdering and cleaning. | |
| Limited | Use an alloy-specific validated cleaning/passivation procedure rather than assuming the stainless standard applies. | |
| Limited | Titanium uses a different descaling or anodic treatment, not this stainless cycle. | |
| No | This chemistry is for stainless steel, not aluminum. | |
| No | Brass is not treated by stainless passivation or pickling baths. | |
| No | Copper alloys use different cleaning and tarnish-control processes. | |
| No | Fused-filament polymers are incompatible with this process. | |
| No | Magnesium is incompatible with these acids. | |
| No | Polymer powder-bed prints are incompatible with this process. | |
| No | Organic polymers cannot take this inorganic metal-finishing process. | |
| No | Photopolymer prints are incompatible with this process. | |
| No | Polymer powder-bed prints are incompatible with this process. | |
| No | Carbon steel is attacked and cannot be passivated by stainless passivation baths. | |
| No | Zinc alloys dissolve in these acids. |
How Stainless passivation is applied, and what it does to the part
- 1Alkaline clean
- 2Rinse
- 3Nitric or citric passivation
- 4Dry
- 5Verification test
| Dimensions | No measurable buildup is expected; the process is suitable for precision threads and fits after compatibility review. |
|---|---|
| Build-up per side | 0 µm — Passivation is a cleaning and surface-conditioning process, not a buildup coating. |
| Masking | Rarely needed. Mask materials attacked by the selected acid and protect trapped assemblies; stainless threads normally need no masking. |
| Electrical | Unchanged |
| Appearance | Normally no visible change on a properly cleaned stainless surface. |
| Added lead time | 2–4 working days on top of the bare part |
Design rules for Stainless passivation
What to decide on the drawing before the part goes to the finisher.
- Specify the governing standard and method.Nitric and citric cycles differ in chemistry, temperature, and safety.
- Remove weld heat tint before passivation.Passivation alone cannot remove thick scale or chromium-depleted metal.
- Use dedicated stainless tooling after treatment.Carbon-steel contact can immediately redeposit free iron.
- Choose an allowed verification test.Passivation quality cannot be confirmed reliably by appearance alone.
Stainless passivation versus the alternatives
Finishes engineers weigh against Stainless passivation, and when each wins.
| Finish | Corrosion | Hardness | Cosmetic | Cost | Thickness | Choose it when |
|---|---|---|---|---|---|---|
Stainless passivation this page | 34 | — | 18 | $ | 0 µm | — |
| 28 | — | 20 | $ | 0 µm | when heat tint or weld scale must be removed before passivating | |
| 45 | — | 82 | $$$ | removes 5–25 µm | when a brighter, smoother, more corrosion-resistant surface is wanted | |
| 34 | — | 18 | $ | 0 µm | when nitric acid handling is not permitted |
The radar overlays Stainless passivation with Stainless Steel Pickling, its most common alternative — chosen when heat tint or weld scale must be removed before passivating. Scores in the table are 0–100 across every finish in the catalog.
Cost, lead time and compliance
Relative cost
Stainless Steel Passivation is a budget-cost finish ($): cheaper than about 94 % of the finishes FabDigit quotes.
Finishing is priced per part with a lot minimum, from FabDigit's own China-side rates cross-checked against US job-shop pricing. The exact figure appears on the instant quote once the part is uploaded.
Lead time and compliance
| Added lead time | 2–4 working days |
|---|---|
| RoHS | Compliant |
| Notes | The finished part is normally RoHS compliant; nitric handling and wastewater controls apply at the processor. |
What Stainless passivation is used for
- Surgical instruments
- Food-processing equipment
- Pharmaceutical vessels
- Marine stainless hardware
Stainless passivation — frequently asked
What is stainless steel passivation?
It chemically removes free iron and lets a chromium-rich oxide film reform. It deposits no measurable coating and normally causes 0 µm buildup.
Nitric vs citric passivation: which is better?
Both can meet ASTM A967 or AMS 2700 when correctly qualified. Citric avoids nitric fumes, while nitric retains broad legacy aerospace approval; the drawing and customer specification decide.
Does passivation change dimensions?
Not measurably in normal processing because no coating is deposited. Precision threads and fits are usually passivated without masking.
Does passivation remove weld discoloration?
No, not reliably. Heavy heat tint and scale require mechanical cleaning or pickling before the passivation cycle.
How do you test stainless passivation?
ASTM A967 permits tests such as water immersion, high humidity, salt spray, copper sulfate, and ferroxyl under stated restrictions. The selected test should match alloy and service.