
Paint, powder & polymer coatings · finish comparison
Electrophoretic Coating vs Powder Coating
Electrophoretic Coating and Powder Coating are both paint, powder & polymer coatings finishes; powder coat is the lower-cost option ($$).
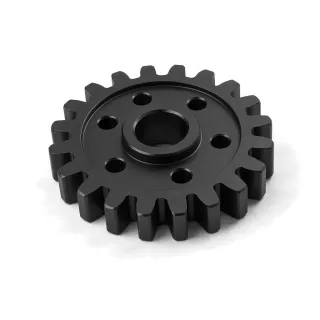
Electrophoretic Coating
Paint, powder & polymer coatings · $$ · instant quote
E-coating deposits a waterborne organic film on an electrically conductive part by electrophoresis.
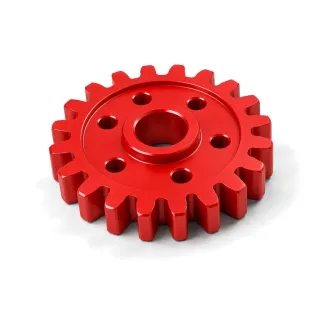
Powder Coating
Paint, powder & polymer coatings · $$ · instant quote
Powder coating electrostatically deposits dry thermoset powder on conductive parts and melts it into a continuous film.
When to choose which
Choose E-coat
Choose E-coat when recess coverage and uniform primer film are more important.
- Typical film thickness is 15–35 µm
- Excellent throwing power reaches recesses and complex frames
- Self-limiting deposition produces comparatively uniform film
Choose Powder coat
Choose Powder coat when thicker decorative topcoat performance is needed.
- Typical finished film is 50–150 µm
- No liquid solvent is needed for film formation
- Tough decorative coverage suits fabricated metal
What the numbers say
- Powder coat is the lower-cost option ($$).
- E-coat is the thinner coating (15–35 µm), so it disturbs tight fits less.
Buyer's decision notes
E-coat is strongest as a controlled immersion-applied corrosion primer on conductive parts, including shapes with recessed surfaces. Powder is strongest as a visible final finish with broad color, gloss and texture choices. They can be complementary layers rather than mutually exclusive substitutes.
- Coverage route
- E-coat reaches conductive surfaces through an immersion bath and electrical deposition; powder is sprayed onto a grounded part. Deep cavities may favor e-coat, while trapped solution, poor drainage, air pockets or inaccessible cleaning paths can still make an immersion route unsuitable.
- Role in the stack
- Decide whether e-coat is the delivered finish or the primer beneath a topcoat. Powder commonly supplies the visible color and texture, while e-coat can supply the corrosion-control base layer on automotive-style systems.
- Geometry and assembly
- Add drain and vent provisions before release, and review seams, hemmed edges, tube ends and threaded inserts. Both routes need electrical contact for processing and a cure cycle that the whole part can tolerate.
- Acceptance
- Qualify the actual stack, pretreatment and substrate. A salt-spray result for one e-coat or powder product does not establish field life for a different film build, edge condition, damage pattern or topcoat combination.
Put this on the RFQ
- State whether the e-coat is a primer or final finish and identify any powder or liquid topcoat over it.
- Mark drain and vent features, rack contacts, cosmetic faces, threads, bond areas and surfaces that must remain bare.
- Specify the coating system, color or topcoat, cure restrictions and the test panel or part locations used for film and adhesion checks.
Primary references
- PPG — Aerocron electrocoat primer — Manufacturer explanation of electrically driven immersion coating, controlled film and coverage of recessed geometry.
- PPG — Powder application process — Manufacturer description of electrostatic powder application, pretreatment and thermal curing.
FabDigit resources: E-coat datasheet · Powder coat datasheet · surface finish selection guide
Scores side by side
Each score is 0–100 against every finish in this catalog. Corrosion is derived from salt-spray test duration and surface hardness from the finish layer's Vickers hardness where a measured figure exists; a finish that leaves the base metal's own surface is not rated for hardness. Cosmetic, lubricity and cost are FabDigit's engineering assessment. Scores and typical figures are screening data, not matched side-by-side tests or service-life rankings; ASTM B117 is a controlled salt-fog method, not a field-life prediction.
| Score | E-coat | Powder coat |
|---|---|---|
| Corrosion resistance | 83 Very good | 83 Very good |
| Surface hardness / wear | 15 Low | 14 Minimal |
| Cosmetic quality | 55 Good | 85 Excellent |
| Lubricity | 15 Low | 15 Low |
| Cost | 35 $$ | 25 $$ |
Key numbers
| Property | E-coat | Powder coat |
|---|---|---|
| Thickness | 15–35 µm | 50–150 µm |
| Salt-spray test duration | 500–1,000 h | 500–1,000 h |
| Max service temperature | 150 °C | 150 °C |
| Electrical | Insulating | Insulating |
| Colours | black, gray, white | RAL colors, custom color, clear |
| Relative cost | Standard ($$) | Standard ($$) |
| Added lead time | 4–8 working days | 3–7 working days |
| RoHS | Compliant | Compliant |
| Instant quote | Yes | Yes |
Bold marks the side that is ahead on a row where more (or less, for cost and lead time) is better. Ranges are the typical specification window; the drawing call-out fixes the class.
Which materials take each finish
| Material family | E-coat | Powder coat |
|---|---|---|
| Aluminum | Yes | Yes |
| Steel | Yes | Yes |
| Brass | With care | With care |
| Copper Alloy | With care | With care |
| DMLS / SLM | With care | With care |
| Magnesium Alloy | With care | With care |
| Stainless Steel | With care | With care |
| Titanium | With care | With care |
| Zinc Alloy | With care | With care |
| FDM | No | Limited |
| MJF | No | Limited |
| Polymer | No | Limited |
| SLA | No | Limited |
| SLS | No | Limited |
E-coat vs Powder coat — frequently asked
What is the difference between E-coat and Powder coat?
Electrophoretic Coating and Powder Coating are both paint, powder & polymer coatings finishes; powder coat is the lower-cost option ($$). E-coat is the thinner coating (15–35 µm), so it disturbs tight fits less.
When should I use E-coat instead of Powder coat?
Choose E-coat when recess coverage and uniform primer film are more important. Conversely: choose Powder coat when thicker decorative topcoat performance is needed.
Is E-coat or Powder coat cheaper?
Powder coat is the lower-cost finish ($$ against $$ for E-coat) among the finishes FabDigit quotes. Both are priced per part with a lot minimum; the exact figure appears on the instant quote once the part is uploaded.
Do E-coat and Powder coat protect equally against corrosion?
On paper, yes: both are rated 500–1,000 h in neutral salt spray (ASTM B117 or the qualification hours of the governing specification). In service the difference comes from sealing, thickness class and the substrate alloy rather than from the choice between the two.