
Anodizing, conversion & passivation · finish comparison
Anodizing Type II vs Chemical Conversion Coating
Anodizing Type II and Chemical Conversion Coating are both anodizing & conversion coatings finishes; type II anodize resists corrosion better (336 h vs 168 h salt spray).
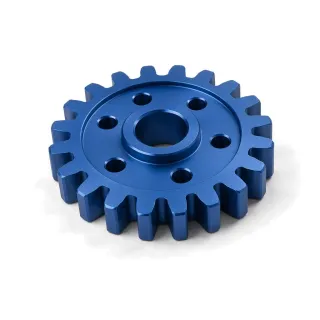
Anodizing Type II
Anodizing & conversion coatings · $$ · instant quote
Type II sulfuric anodizing converts aluminum into a porous aluminum-oxide coating that can be clear or dyed.
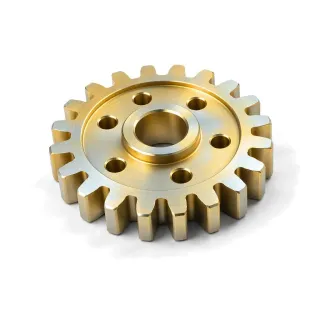
Chemical Conversion Coating
Anodizing & conversion coatings · $ · instant quote
Chem film is a thin chemical conversion coating for aluminum that improves corrosion resistance while retaining useful electrical conductivity.
When to choose which
Choose Type II anodize
Choose Type II anodize when greater wear resistance and decorative color are required.
- Provides a hard 200–400 HV oxide
- Supports clear and many dyed colors
- Sealed coatings meet a 336-hour ASTM B117 requirement under MIL-A-8625
Choose Chem film
Choose Chem film when electrical conductivity is required.
- Adds essentially no dimensional change (typically well under 1 µm)
- Class 3 preserves low-resistance grounding surfaces
- Class 1A improves paint and primer adhesion
What the numbers say
- Type II anodize resists corrosion better (336 h vs 168 h salt spray).
- Chem film is the lower-cost option ($).
- Chem film is the thinner coating (0.1–1.5 µm), so it disturbs tight fits less.
- Type II anodize is insulating; Chem film is conductive.
Buyer's decision notes
Use Type II anodize when the aluminum surface itself must provide the visible, wear-bearing finish. Use chemical conversion coating when the priority is a paint or adhesive pretreatment, a very light-touch conversion layer, or an electrical contact area that must remain conductive.
- Substrate and appearance
- Both routes are for aluminum and aluminum alloys. Anodize is the stronger cosmetic choice when color and a finished exposed surface matter; chem film is usually selected for functional protection, bonding or a later coating system.
- Fits and contacts
- Treat anodize thickness and dimensional buildup as separate drawing decisions: the process both consumes and grows the aluminum surface. Mask bearing seats, threads, grounding pads and contact lands when the finished interface cannot accept the coating or its electrical resistance.
- Electrical path
- Do not describe chem film as conductive without a class and a contact-resistance requirement. MIL-DTL-5541 Class 3 is the electrical-contact route, but the acquisition document still has to state the test method and acceptance value for the application.
- Corrosion evidence
- A salt-spray qualification demonstrates a controlled coating system; it does not predict calendar life in a particular marine, outdoor or galvanic assembly. Alloy, pretreatment, sealing, damage and mating metals still control service behavior.
Put this on the RFQ
- State the aluminum alloy and temper, MIL specification, Type or Class, color, seal and any approved chemistry restrictions.
- Mark electrical contacts, threaded features, bearing fits, bond lands and cosmetic faces on the drawing instead of relying on a blanket “mask as required” note.
- If chem film is a pretreatment, identify the complete paint or adhesive system and the allowed time or handling condition before the next operation.
Primary references
- DLA ASSIST — MIL-PRF-8625 — Active performance specification for Type II and Type III anodic coatings on aluminum and aluminum alloys.
- DLA ASSIST — MIL-DTL-5541 — Active detail specification for chemical conversion coatings on aluminum and aluminum alloys.
FabDigit resources: Type II anodize datasheet · Chem film datasheet · surface finish selection guide
Scores side by side
Each score is 0–100 against every finish in this catalog. Corrosion is derived from salt-spray test duration and surface hardness from the finish layer's Vickers hardness where a measured figure exists; a finish that leaves the base metal's own surface is not rated for hardness. Cosmetic, lubricity and cost are FabDigit's engineering assessment. Scores and typical figures are screening data, not matched side-by-side tests or service-life rankings; ASTM B117 is a controlled salt-fog method, not a field-life prediction.
| Score | Type II anodize | Chem film |
|---|---|---|
| Corrosion resistance | 71 Very good | 60 Good |
| Surface hardness / wear | 54 Fair | — — |
| Cosmetic quality | 88 Excellent | 35 Fair |
| Lubricity | 18 Low | 12 Minimal |
| Cost | 24 $$ | 15 $ |
Key numbers
| Property | Type II anodize | Chem film |
|---|---|---|
| Thickness | 5–25 µm | 0.1–1.5 µm |
| Surface hardness | 200–400 HV | — |
| Salt-spray test duration | 336 h | 168 h |
| Max service temperature | 80 °C | 80 °C |
| Electrical | Insulating | Conductive |
| Colours | clear, black, red, blue, gold, custom dye | clear, gold, iridescent |
| Relative cost | Standard ($$) | Budget ($) |
| Added lead time | 3–5 working days | 2–4 working days |
| RoHS | Compliant | Conditional |
| Instant quote | Yes | Yes |
Bold marks the side that is ahead on a row where more (or less, for cost and lead time) is better. Ranges are the typical specification window; the drawing call-out fixes the class.
Which materials take each finish
| Material family | Type II anodize | Chem film |
|---|---|---|
| Aluminum | Yes | Yes |
| DMLS / SLM | With care | With care |
Specifications and drawing call-outs
Type II anodize
- MIL-A-8625 — Anodic Coatings for Aluminum and Aluminum Alloys
- AMS 2471 — Anodic Treatment of Aluminum Alloys, Sulfuric Acid Process, Undyed Coating
- AMS 2472 — Anodic Treatment of Aluminum Alloys, Sulfuric Acid Process, Dyed Coatings
- ISO 7599 — Anodizing of Aluminium and Its Alloys — Method for Specifying Decorative and Protective Anodic Oxidation Coatings on Aluminium
ANODIZE PER MIL-A-8625 TYPE II CLASS 2, BLACK, 0.0005 IN THICK; MASK ALL THREADS AND ELECTRICAL CONTACTS
Chem film
- MIL-DTL-5541 — Chemical Conversion Coatings on Aluminum and Aluminum Alloys
CHEMICAL CONVERSION COAT PER MIL-DTL-5541, TYPE II, CLASS 3, CLEAR; MASK THREADED CONTACT STUDS
Type II anodize vs Chem film — frequently asked
What is the difference between Type II anodize and Chem film?
Anodizing Type II and Chemical Conversion Coating are both anodizing & conversion coatings finishes; type II anodize resists corrosion better (336 h vs 168 h salt spray). Chem film is the lower-cost option ($). Chem film is the thinner coating (0.1–1.5 µm), so it disturbs tight fits less.
When should I use Type II anodize instead of Chem film?
Choose Type II anodize when greater wear resistance and decorative color are required. Conversely: choose Chem film when electrical conductivity is required.
Is Type II anodize or Chem film cheaper?
Chem film is the lower-cost finish ($ against $$ for Type II anodize) among the finishes FabDigit quotes. Both are priced per part with a lot minimum; the exact figure appears on the instant quote once the part is uploaded.
Which lasts longer in salt spray, Type II anodize or Chem film?
Type II anodize. Type II anodize is rated 336 h and Chem film 168 h in neutral salt spray (ASTM B117 or the qualification hours of the governing specification). The figures are for the finish as specified on a clean, properly pre-treated substrate; sealing, thickness class and substrate alloy move them.